Category: Track and Trace System

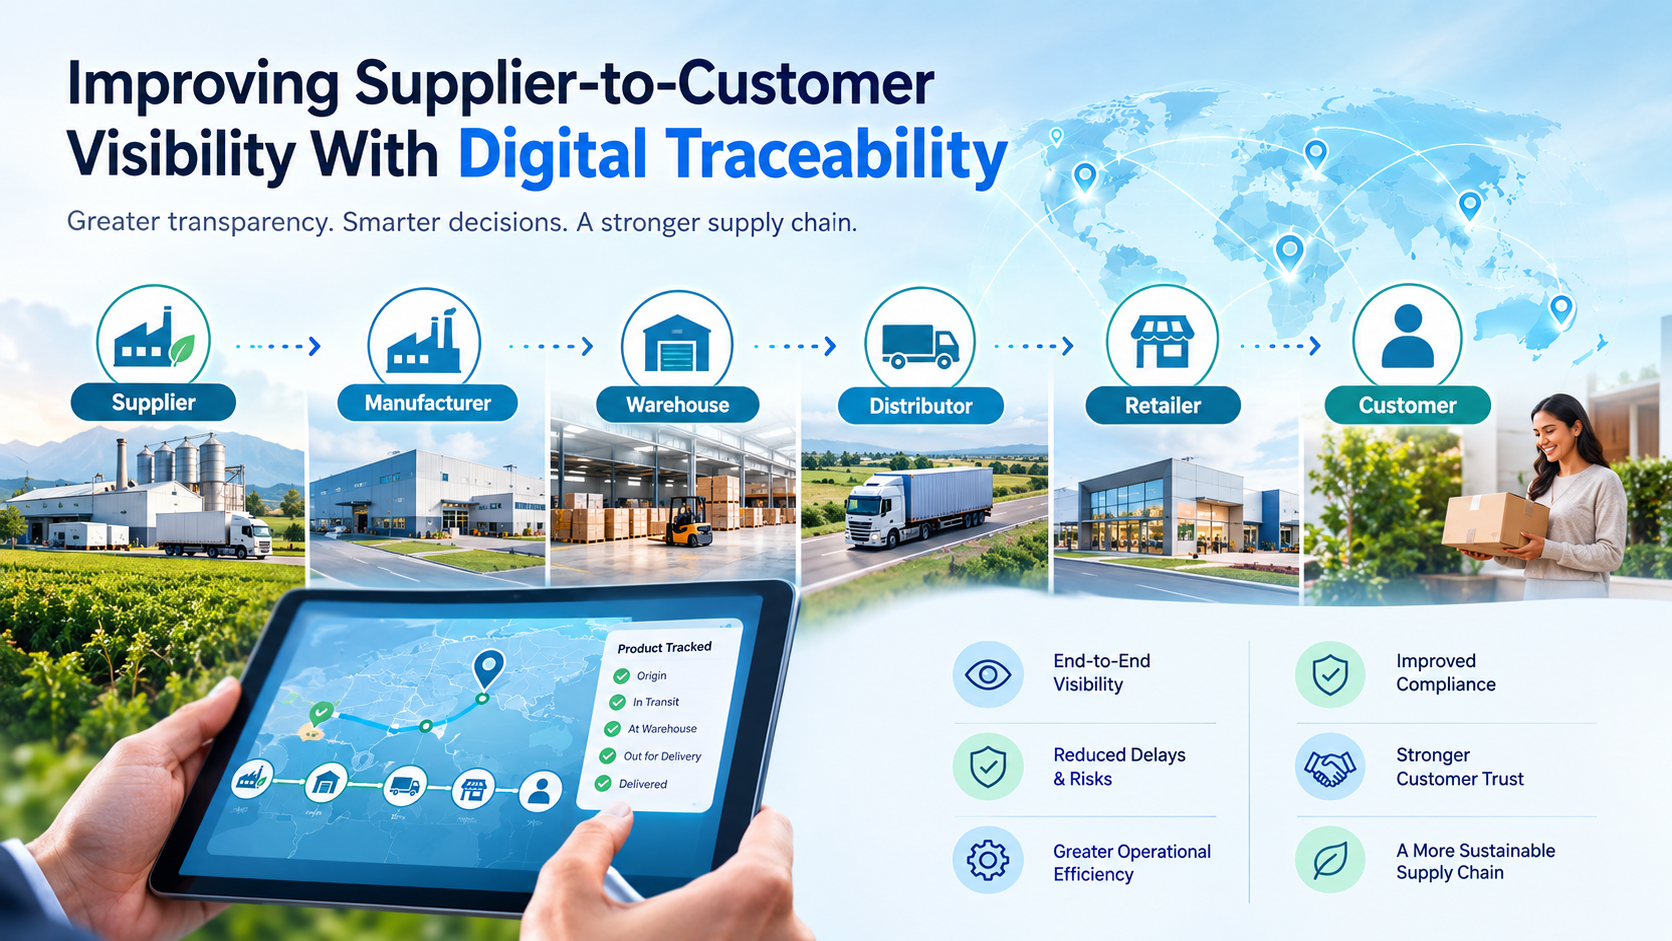
  • Improving Supplier-to-Customer Visibility With Digital Traceability

    Improving Supplier-to-Customer Visibility With Digital Traceability

    Improving Supplier-to-Customer Visibility With Digital Traceability

    Modern supply chains involve multiple suppliers, manufacturers, warehouses, distributors, retailers, and customers. With so many parties involved, it can become difficult for businesses to know where products are, what is happening to them, and whether they are moving according to plan.

    Digital traceability helps solve this problem by providing businesses with better visibility into products, materials, shipments, and processes throughout the supply chain. By collecting and connecting data at different stages, companies can improve transparency, identify problems faster, and provide customers with more reliable information.

    What Is Digital Traceability in the Supply Chain?

    Digital traceability is the process of using digital technologies to track and record the movement of products, materials, and information throughout the supply chain.

    Instead of depending on manual records or disconnected systems, businesses can use technologies such as RFID, barcodes, IoT sensors, cloud platforms, and data analytics to create a connected view of their supply chain.

    How Digital Traceability Works

    Digital traceability begins when a product or raw material enters the supply chain. A unique identifier, such as a barcode, QR code, or RFID tag, can be assigned to the item.

    As the product moves between suppliers, manufacturers, warehouses, distributors, and retailers, important information can be recorded at different points.

    This information may include:

    • Product identification
    • Supplier information
    • Manufacturing details
    • Location
    • Shipment status
    • Inventory information
    • Temperature or environmental conditions
    • Delivery information

    The collected information can then be stored and analyzed through digital platforms, giving businesses greater visibility into their supply chain.

    Why Supply Chain Traceability Matters

    Without proper traceability, businesses may struggle to identify where a product came from, where it is currently located, or what happened during transportation.

    Digital traceability creates a record of important supply chain activities. This can help businesses investigate problems, improve operations, support compliance, and provide customers with more accurate product information.

    Why Supplier-to-Customer Visibility Is Important

    Supplier-to-customer visibility means having a clear understanding of what happens to products and materials from the supplier stage through the final customer.

    When information is available across the supply chain, businesses can make decisions based on current and reliable data.

    Improving Supply Chain Transparency

    A connected supply chain allows businesses to see information from different stages in one place.

    For example, a manufacturer can monitor incoming materials from suppliers, production progress, warehouse inventory, and outgoing shipments. This creates greater transparency between different supply chain participants.

    Reducing Delays and Operational Risks

    Supply chain delays can happen because of transportation problems, inventory shortages, production issues, or communication gaps.

    Digital traceability can help businesses identify where a delay has occurred and provide information that supports faster investigation and response.

    Building Customer Trust

    Customers increasingly want to know where products come from and how they reach them.

    Providing accurate product and shipment information can improve transparency and help businesses build stronger relationships with customers.

    How Digital Traceability Improves Supplier-to-Customer Visibility

    Digital traceability connects information from different points in the supply chain and makes that information easier to access and analyze.

    Tracking Products Across the Supply Chain

    Businesses can use barcodes, QR codes, RFID tags, and IoT devices to track products as they move through different stages.

    This allows organizations to understand product movement from the supplier to manufacturing, warehousing, distribution, and delivery.

    Connecting Suppliers, Manufacturers, and Distributors

    Supply chain visibility becomes difficult when each business partner uses separate systems.

    Digital platforms can help connect information from suppliers, manufacturers, logistics providers, distributors, and other stakeholders. This reduces information gaps and makes collaboration easier.

    Providing Real-Time Supply Chain Data

    Traditional supply chain records may depend on manual updates, which can result in outdated information.

    Connected technologies can automatically capture and update information as products move through the supply chain. This gives businesses a more current view of inventory, shipments, and product status.

    Improving Product and Shipment Traceability

    Digital traceability creates a digital record of important product and shipment activities.

    If an issue occurs, businesses can use this information to identify affected products, locations, suppliers, or shipments more efficiently.

    Key Technologies Used for Digital Traceability

    Several technologies can work together to create an effective digital traceability system.

    RFID and Barcode Tracking

    RFID tags and barcodes are commonly used to identify and track products, packages, assets, and inventory.

    Barcodes generally require scanning, while RFID technology can allow identification without direct line-of-sight in suitable environments.

    IoT Sensors and Connected Devices

    IoT devices can collect information about products, vehicles, warehouses, and environmental conditions.

    For example, sensors can monitor temperature, humidity, location, or movement during transportation. This information can be useful when products require specific storage or transportation conditions.

    Cloud-Based Supply Chain Platforms

    Cloud platforms can bring supply chain information together in a centralized environment.

    Authorized users can access relevant information from different locations, helping suppliers, manufacturers, logistics providers, and businesses collaborate more effectively.

    Data Analytics and Artificial Intelligence

    Supply chain data can be analyzed to identify patterns, inefficiencies, and potential problems.

    AI and analytics can help businesses understand historical data, detect unusual activity, forecast demand, and support supply chain decision-making.

    Blockchain for Supply Chain Transparency

    Blockchain can provide a distributed record of selected supply chain transactions.

    When appropriately implemented, it can help different stakeholders share and verify certain records while maintaining a history of transactions.

    Benefits of Digital Traceability for Businesses

    Implementing digital traceability can provide benefits across different areas of supply chain operations.

    Better Inventory Visibility

    Businesses can gain a clearer understanding of inventory levels and product locations.

    Better visibility can help organizations identify stock discrepancies, improve inventory planning, and reduce unnecessary delays.

    Faster Identification of Supply Chain Issues

    When information is collected across multiple supply chain stages, businesses can investigate problems more efficiently.

    For example, if a shipment is delayed, tracking information can help identify its last known location and relevant events.

    Improved Regulatory Compliance

    Many industries require businesses to maintain records related to products, materials, manufacturing, transportation, and distribution.

    Digital traceability can help organizations maintain organized records and retrieve relevant information when required.

    Reduced Product Loss and Errors

    Automated identification and tracking can reduce dependence on manual data entry.

    More accurate product information can help reduce issues such as misplaced inventory, incorrect shipments, and tracking errors.

    Better Customer Experience

    Customers can benefit from accurate delivery information, product details, and greater transparency.

    Businesses can also respond to customer questions more quickly when relevant supply chain information is readily available.

    How to Implement Digital Traceability

    A successful digital traceability strategy requires more than simply adding a tracking technology. Businesses need to consider their processes, systems, data, and supply chain partners.

    Identify Supply Chain Visibility Gaps

    Start by identifying where information is currently missing or difficult to access.

    Businesses should examine supplier management, production, warehousing, transportation, distribution, and customer delivery processes.

    Select the Right Tracking Technologies

    The appropriate technology depends on the type of products, operating environment, budget, and tracking requirements.

    Businesses may use barcodes, RFID, QR codes, IoT sensors, GPS, cloud platforms, or a combination of technologies.

    Integrate Supplier and Customer Data

    Traceability becomes more useful when information from different systems can work together.

    Integration can connect supplier information with manufacturing, warehouse, logistics, and customer-facing systems.

    Monitor and Analyze Supply Chain Data

    Collecting data is only the first step. Businesses should regularly analyze the information to identify delays, inventory issues, process inefficiencies, and other supply chain problems.

    Continuously Improve Traceability Processes

    Supply chains change over time. Businesses should regularly review their traceability systems and update processes as new technologies, suppliers, products, and customer requirements emerge.

    Challenges of Implementing Digital Traceability

    Although digital traceability offers significant operational benefits, implementation can involve several challenges.

    Data Integration Challenges

    Different suppliers and business partners may use different software platforms and data formats.

    Connecting these systems can require integration work and standardized data processes.

    Technology and Implementation Costs

    Businesses may need to invest in hardware, software, sensors, integration, training, and maintenance.

    The implementation strategy should therefore be aligned with the organization’s operational requirements and available resources.

    Supplier Adoption and Collaboration

    A supply chain involves multiple organizations. If suppliers or logistics partners do not share the required information, complete visibility can be difficult to achieve.

    Clear processes and communication between stakeholders are important for successful implementation.

    Data Security and Privacy

    Digital traceability systems handle large amounts of business and operational information.

    Organizations should use appropriate access controls, security practices, and data management policies to protect sensitive information.

    Future of Digital Traceability in Supply Chains

    Digital traceability is expected to become increasingly connected as businesses adopt technologies such as AI, IoT, cloud computing, and advanced analytics.

    AI-Powered Supply Chain Visibility

    AI can help organizations analyze large amounts of supply chain data and identify patterns that may be difficult to detect manually.

    Businesses can use these insights to support planning, risk management, and operational decision-making.

    Real-Time IoT Tracking

    IoT devices can provide continuous information about products, vehicles, assets, and environmental conditions.

    As connected devices become more widely adopted, businesses can develop more detailed views of supply chain activities.

    Predictive Supply Chain Analytics

    Instead of only understanding what has already happened, businesses can use historical and current data to identify potential future issues.

    Predictive analytics can support areas such as demand planning, inventory management, transportation, and maintenance.

    Increasing Demand for End-to-End Traceability

    Customers, regulators, and business partners are placing greater importance on transparency and product information.

    This is increasing the need for businesses to develop traceability systems that connect different stages of the supply chain.

    Conclusion

    Improving supplier-to-customer visibility requires businesses to connect information across the entire supply chain. Digital traceability provides a practical way to track products, capture important data, and improve transparency from suppliers to final customers.

    By combining technologies such as RFID, barcodes, IoT, cloud platforms, and analytics, businesses can develop a more connected view of their operations. This can support better inventory management, faster issue identification, improved transparency, and a better customer experience.

    As supply chains become more complex, digital traceability can play an important role in helping businesses create more connected, transparent, and data-driven supply chain operations.

    Frequently Asked Questions About Digital Traceability

    Q1. What is digital traceability?

    Digital traceability is the use of digital technologies to track and record products, materials, and processes as they move through different stages of the supply chain.

    Q2. How does digital traceability improve supply chain visibility?

    It connects information from suppliers, manufacturers, warehouses, logistics providers, distributors, and other supply chain stages, giving businesses a more complete view of product movement and status.

    Q3. What technologies are used for supply chain traceability?

    Common technologies include RFID, barcodes, QR codes, IoT sensors, GPS, cloud platforms, data analytics, and artificial intelligence.

    Q4. What are the benefits of digital traceability?

    Digital traceability can improve supply chain transparency, inventory visibility, product tracking, issue identification, compliance management, and customer communication.

    Q5. How can businesses implement digital traceability?

    Businesses can begin by identifying visibility gaps, selecting appropriate tracking technologies, integrating supply chain systems, establishing data standards, and continuously monitoring performance.
  • How Supply Chain Traceability Works Across Multiple Suppliers

    How Supply Chain Traceability Works Across Multiple Suppliers

    How Supply Chain Traceability Works Across Multiple Suppliers

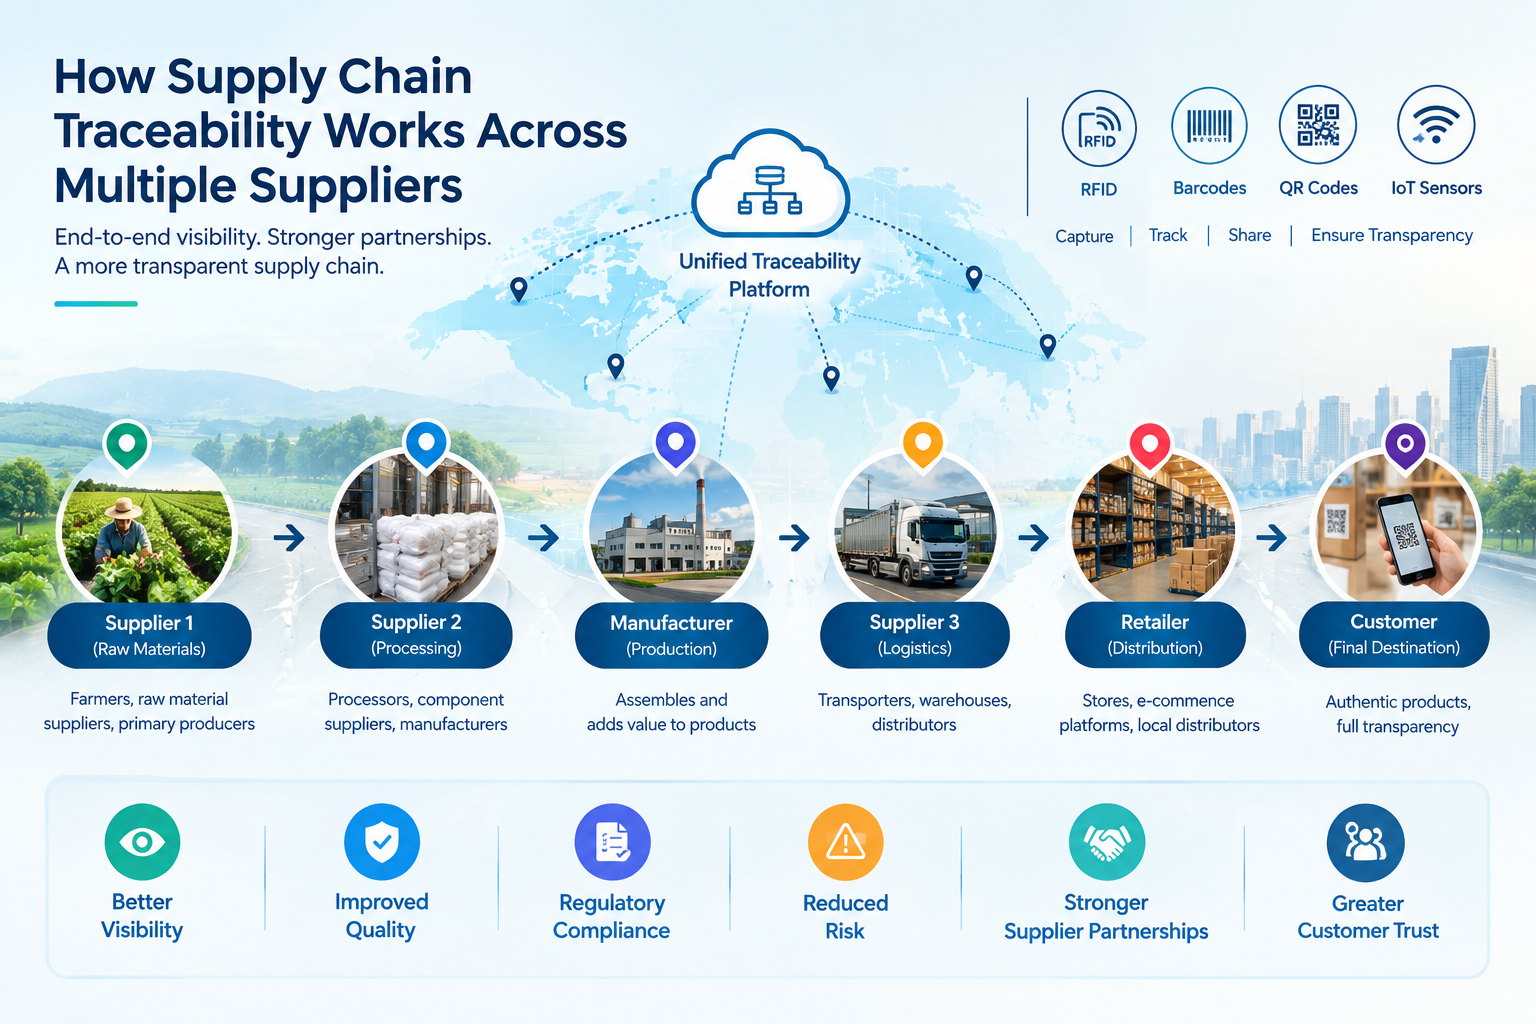
    Modern supply chains rarely depend on a single supplier. Manufacturers, distributors, retailers, and logistics providers often work with multiple vendors across different regions. While this improves flexibility and sourcing options, it also creates challenges in tracking products, materials, and information. This is where supply chain traceability becomes essential.

    Supply chain traceability allows businesses to monitor the movement of products, raw materials, and components from the source to the final customer. It provides complete visibility across all suppliers, helping organizations improve quality, ensure compliance, reduce risks, and build customer trust.

    What Is Supply Chain Traceability?

    Supply chain traceability is the process of recording, tracking, and monitoring products and materials throughout every stage of the supply chain. It enables businesses to identify where products come from, how they are processed, and where they are delivered.

    For companies working with multiple suppliers, traceability creates a connected view of supplier information, inventory, production, transportation, and delivery data.

    How Supply Chain Traceability Works Across Multiple Suppliers

    When several suppliers contribute materials or components, businesses need a structured system to collect and share information.

    Supplier Identification and Data Collection

    The first step is collecting data from every supplier. This includes:

    • Supplier details
    • Product information
    • Batch or lot numbers
    • Manufacturing dates
    • Shipping records
    • Compliance documents

    A centralized traceability platform stores this information and creates a digital record for every product.

    Tracking Materials From Source to Manufacturer

    Raw materials often pass through multiple suppliers before reaching manufacturers. Each movement is recorded using tracking technologies such as RFID tags, barcodes, QR codes, or IoT sensors.

    For example, a food manufacturer may source ingredients from different farms, processors, and packaging suppliers. Traceability systems connect data from every supplier to create an end-to-end product history.

    Connecting Data Across Multiple Supply Chain Partners

    A major challenge in multi-supplier environments is integrating data from different systems. Cloud-based traceability platforms help businesses combine information from suppliers, warehouses, transport providers, and production units into a single dashboard.

    This improves visibility and allows organizations to track products in real time.

    Using RFID, Barcodes, QR Codes, and IoT

    Several technologies support supply chain traceability:

    • RFID: Enables automatic product identification and tracking.
    • Barcodes: Provide cost-effective item tracking.
    • QR Codes: Offer detailed product information and easy scanning.
    • IoT Sensors: Monitor location, temperature, humidity, and movement.

    These technologies improve data accuracy and reduce manual errors.

    Real-Time Supply Chain Visibility

    Real-time visibility helps businesses identify delays, shortages, and quality issues quickly. Managers can monitor supplier performance, inventory levels, and shipment status through digital dashboards.

    This reduces disruptions and improves operational efficiency.

    Key Components of Multi-Supplier Supply Chain Traceability

    An effective traceability system includes several essential elements:

    Supplier Data Management

    Maintaining accurate supplier records is critical for traceability.

    Product and Batch Tracking

    Tracking batches allows businesses to identify affected products during recalls or quality issues.

    Digital Traceability Records

    Digital records improve transparency and simplify audits.

    Data Integration and Sharing

    Connected systems enable smooth communication between suppliers and business partners.

    Real-Time Monitoring and Alerts

    Automated alerts help businesses respond quickly to disruptions.

    Benefits of Supply Chain Traceability Across Multiple Suppliers

    Businesses gain several advantages from implementing traceability systems.

    Better Supply Chain Visibility

    Organizations can monitor products and materials at every stage.

    Faster Problem Identification

    Issues can be detected and resolved quickly.

    Improved Product Quality

    Better monitoring leads to consistent quality standards.

    Easier Regulatory Compliance

    Traceability supports compliance with industry regulations.

    Reduced Supply Chain Risk

    Companies can identify supplier risks and minimize disruptions.

    Improved Customer Trust

    Customers increasingly expect transparency regarding product origin and quality.

    Challenges of Tracking Multiple Suppliers

    Despite its benefits, multi-supplier traceability presents challenges.

    Inconsistent Supplier Data

    Different suppliers may use different formats and systems.

    Lack of Data Integration

    Disconnected systems can limit visibility.

    Limited Supply Chain Transparency

    Incomplete information can affect decision-making.

    Supplier Compliance Issues

    Not all suppliers maintain the same standards.

    Managing Large Volumes of Data

    Businesses need efficient systems to handle traceability information.

    Technologies Used for Multi-Supplier Traceability

    Several digital technologies strengthen traceability systems:

    RFID Technology

    Automates product identification and tracking.

    Barcode and QR Code Tracking

    Supports cost-effective inventory management.

    IoT Sensors

    Provide real-time monitoring.

    Cloud-Based Platforms

    Enable centralized data management.

    AI and Analytics

    Help predict risks and improve decision-making.

    Best Practices for Implementing Supply Chain Traceability

    To improve traceability across multiple suppliers, businesses should:

    • Standardize supplier data.
    • Integrate supply chain systems.
    • Automate data collection.
    • Monitor supplier performance.
    • Use real-time tracking technologies.
    • Maintain accurate digital records.

    Frequently Asked Questions

    Q1. What is supply chain traceability?

    Supply chain traceability is the ability to track products, materials, and information throughout the supply chain.

    Q2. How does traceability work across multiple suppliers?

    It combines supplier, inventory, production, and logistics data into a unified system.

    Q3. Which technologies support traceability?

    RFID, barcodes, QR codes, IoT sensors, cloud platforms, and AI are commonly used.

    Conclusion

    Supply chain traceability across multiple suppliers provides organizations with greater visibility, better quality control, and improved compliance. By connecting supplier data with technologies such as RFID, barcodes, IoT, and cloud platforms, businesses can build transparent and resilient supply chains. As global supply networks continue to grow, traceability will remain a key factor in improving efficiency, reducing risks, and strengthening customer trust.

  • B. Supply Chain Traceability

    B. Supply Chain Traceability

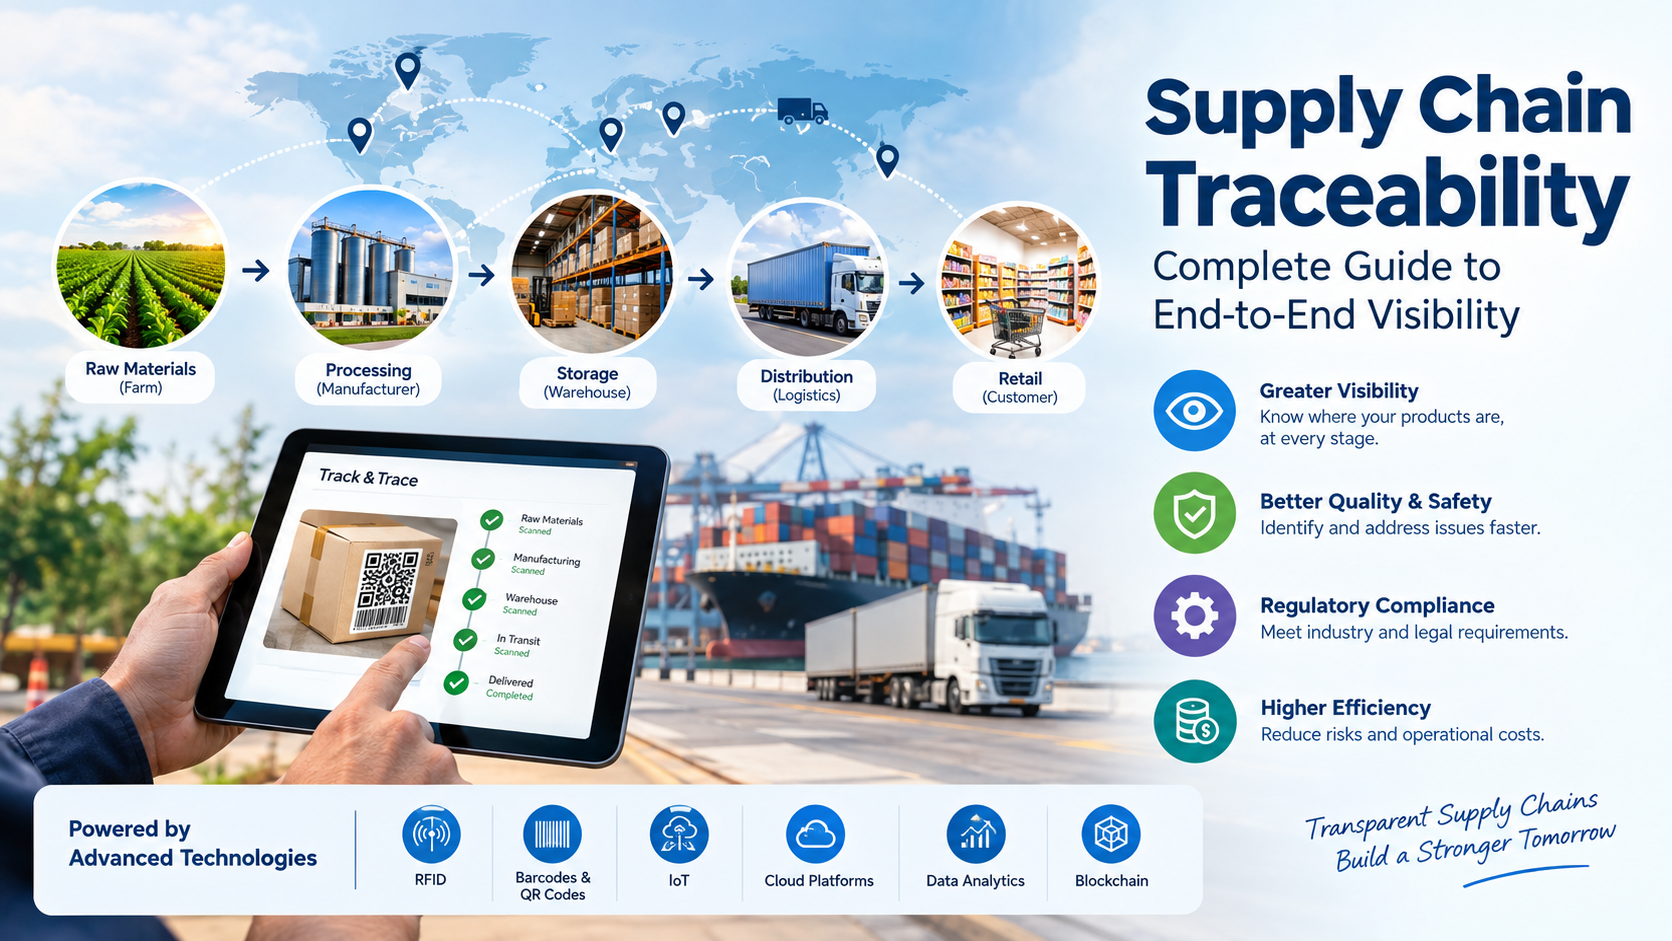
    Supply Chain Traceability: A Complete Guide to End-to-End Visibility

    Supply chains have become more complex as businesses source materials, manufacture products, and deliver goods across multiple locations. With so many stages involved, companies need to know where products come from, where they are currently located, and what happens to them throughout their journey.

    Supply chain traceability helps businesses track products, materials, and information from the point of origin to the final customer. By using technologies such as RFID, barcodes, IoT, cloud platforms, and data analytics, organizations can improve visibility, identify problems faster, and make better supply chain decisions.

    In this guide, we will explain what supply chain traceability is, how it works, its benefits, key technologies, challenges, and how businesses can implement a traceability system.

    What Is Supply Chain Traceability?

    Supply chain traceability is the ability to track and document the movement of products, materials, components, and related information throughout the supply chain.

    It creates a record of where a product comes from, what processes it goes through, where it moves, and where it ultimately reaches. This information can help businesses understand their supply chain and respond quickly when problems occur.

    For example, a manufacturer may use traceability to track raw materials from a supplier, monitor production, record warehouse movements, and track the finished product during distribution.

    How Supply Chain Traceability Works

    A typical traceability process includes:

    1. Identifying products or materials.
    2. Capturing information at different supply chain stages.
    3. Recording and storing the data.
    4. Tracking movement between locations.
    5. Monitoring products in real time where required.
    6. Using the collected information for analysis and decision-making.

    The exact process depends on the industry, product type, regulatory requirements, and technology used.

    Why Supply Chain Traceability Matters

    Without proper traceability, businesses may have difficulty identifying where a product came from or where a problem occurred.

    Traceability can help organizations:

    • Improve supply chain visibility
    • Track products and materials
    • Identify quality problems
    • Support product recalls
    • Improve inventory management
    • Meet regulatory requirements
    • Reduce operational risks
    • Provide customers with better product information

    How Does Supply Chain Traceability Work?

    Supply chain traceability connects information collected at different stages of the product lifecycle.

    Product Identification and Data Capture

    Products, packages, assets, and materials can be identified using barcodes, QR codes, RFID tags, serial numbers, or other identification methods.

    Information such as product ID, batch number, manufacturing date, location, and shipment details can then be captured and stored.

    Tracking Products Across the Supply Chain

    After identification, products can be tracked as they move between suppliers, factories, warehouses, distribution centers, retailers, and customers.

    This provides businesses with greater visibility into product movement and inventory status.

    Data Integration and Monitoring

    A traceability system can connect information from different business systems, including ERP, WMS, manufacturing, logistics, and inventory platforms.

    Integration helps create a more connected view of supply chain activities.

    Traceability Data Analysis

    Collected data can be analyzed to identify delays, inventory issues, quality problems, and other operational challenges.

    Businesses can use these insights to improve processes and make informed decisions.

    Key Components of Supply Chain Traceability

    An effective traceability system typically combines identification technologies, data collection, software, and analytics.

    RFID and Barcode Technology

    RFID tags and barcodes are widely used to identify and track products, packages, pallets, and assets.

    Barcodes generally require scanning, while RFID can allow compatible systems to identify tagged items without direct line-of-sight scanning.

    IoT and Real-Time Tracking

    IoT devices and sensors can collect information about location, temperature, humidity, movement, and other conditions.

    This can be particularly useful for products that require controlled transportation or storage.

    Cloud-Based Traceability Systems

    Cloud platforms can centralize supply chain information and make data accessible to authorized users across different locations.

    They can also support integration, reporting, and collaboration between supply chain partners.

    Data Integration and Analytics

    Integration connects traceability information with existing business systems.

    Analytics tools can then help organizations identify patterns, monitor performance, and investigate supply chain events.

    Benefits of Supply Chain Traceability

    Implementing supply chain traceability can provide operational and strategic benefits.

    Improved Supply Chain Visibility

    Traceability provides businesses with information about product movement and supply chain events.

    Better visibility can help teams understand what is happening across different stages of the supply chain.

    Better Product Quality and Safety

    Businesses can track batches, materials, and production information to help identify potential quality problems.

    If an issue is discovered, traceability data can help determine which products or batches may be affected.

    Faster Identification of Issues

    When supply chain problems occur, organizations can use traceability records to investigate where and when an issue happened.

    This can reduce the time required for root cause analysis.

    Improved Regulatory Compliance

    Many industries have specific requirements for product tracking, documentation, safety, and reporting.

    A structured traceability system can help businesses maintain the information required to support compliance processes.

    Reduced Operational Costs

    Better visibility can help organizations identify inefficiencies, reduce manual processes, improve inventory management, and minimize errors.

    The actual cost savings depend on the business process and implementation.

    Supply Chain Traceability Across Different Industries

    Traceability is used across industries where businesses need visibility into products, materials, and processes.

    Food and Agriculture

    Food businesses can use traceability to track ingredients, batches, processing activities, storage conditions, and distribution.

    This can support food safety investigations and product recalls.

    Pharmaceuticals and Healthcare

    Pharmaceutical supply chains require detailed information about products, batches, storage, and distribution.

    Traceability can help organizations monitor products throughout their supply chain.

    Manufacturing

    Manufacturers can track raw materials, components, production stages, finished goods, and shipments.

    This can support quality management and production visibility.

    Retail and E-commerce

    Retailers can use traceability to track products from suppliers through distribution centers and stores or directly to customers.

    It can also support inventory visibility and product authentication processes.

    Logistics and Transportation

    Logistics companies can use tracking technologies to monitor shipments, vehicles, containers, and other assets.

    This can provide greater visibility into transportation activities.

    Technologies Used in Supply Chain Traceability

    Modern traceability systems often combine several technologies rather than relying on a single solution.

    RFID

    Radio Frequency Identification uses tags and readers to identify and track objects.

    RFID can be useful for inventory, warehouse, asset, and logistics applications.

    Barcodes and QR Codes

    Barcodes and QR codes provide a practical way to identify products and connect them with digital information.

    They are widely used because they can be relatively simple to deploy and operate.

    Internet of Things (IoT)

    IoT sensors can collect information from physical objects and environments.

    Businesses can use this information for location monitoring, condition monitoring, and real-time visibility.

    Artificial Intelligence and Analytics

    AI and analytics can help businesses analyze large volumes of supply chain data.

    Potential applications include demand analysis, anomaly detection, risk monitoring, and predictive insights.

    Blockchain

    Blockchain can provide a distributed record of transactions between participating organizations.

    In some supply chain applications, it can support data sharing and record verification. However, blockchain is not required for every traceability implementation.

    Challenges of Supply Chain Traceability

    Although traceability provides significant visibility, implementation can also present challenges.

    Data Accuracy and Quality

    Traceability depends on accurate data. Incorrect, incomplete, or delayed information can reduce the usefulness of the system.

    Businesses need appropriate processes for data capture and validation.

    Integration With Existing Systems

    Companies may already use ERP, warehouse, manufacturing, logistics, or inventory systems.

    Connecting these systems with a traceability platform can require technical planning and integration work.

    Implementation Costs

    Hardware, software, integration, training, and maintenance can contribute to implementation costs.

    Organizations should evaluate their requirements and choose a solution that fits their operational needs.

    Lack of Supply Chain Visibility

    Businesses often work with multiple suppliers, logistics providers, and partners.

    Getting consistent data from different organizations can be challenging and may require common standards and collaboration.

    How to Implement a Supply Chain Traceability System

    Businesses should approach traceability as a structured process rather than simply installing tracking technology.

    Identify Traceability Requirements

    Start by identifying what needs to be tracked.

    This could include raw materials, components, finished products, shipments, assets, batches, or environmental conditions.

    Select the Right Technology

    Choose identification and tracking technologies based on the business requirements.

    Depending on the use case, this could include RFID, barcodes, QR codes, IoT sensors, GPS, cloud platforms, or analytics tools.

    Integrate Supply Chain Data

    Connect the traceability platform with relevant business systems.

    Integration can help create a consistent flow of information between suppliers, warehouses, production facilities, logistics operations, and other stakeholders.

    Monitor and Improve the System

    After implementation, businesses should regularly monitor data quality, system performance, user adoption, and operational results.

    Traceability systems can be improved over time as business requirements change.

    Future of Supply Chain Traceability

    Supply chains are becoming increasingly connected and data-driven.

    AI-Powered Traceability

    AI can help organizations analyze large volumes of supply chain data and identify unusual patterns, risks, or potential disruptions.

    Real-Time Supply Chain Visibility

    IoT devices, connected systems, and cloud platforms are enabling businesses to collect and share supply chain information more quickly.

    Digital Product Passports

    Digital product passports can provide structured information about products, materials, and lifecycle-related data.

    They may become increasingly relevant for organizations that need greater product transparency.

    Connected and Intelligent Supply Chains

    The future of traceability is likely to involve greater integration between physical products, digital systems, sensors, analytics, and supply chain partners.

    This can help businesses move toward more connected and responsive supply chain operations.

    Conclusion

    Supply chain traceability provides businesses with greater visibility into the movement and history of products, materials, and assets. By combining technologies such as RFID, barcodes, IoT, cloud platforms, and analytics, organizations can build more connected and transparent supply chains.

    As supply chains become more complex, traceability can help businesses understand their operations, respond to issues, improve processes, and provide better information to customers and supply chain partners.

    For organizations looking to improve supply chain visibility, implementing a traceability strategy based on their specific products, processes, and business requirements can be an important step toward a more connected supply chain.

    Frequently Asked Questions About Supply Chain Traceability

    Q1. What is supply chain traceability?

    Supply chain traceability is the ability to track products, materials, and related information throughout different stages of the supply chain, from origin to final destination.

    Q2. Why is supply chain traceability important?

    It can help businesses improve visibility, investigate quality issues, manage recalls, support compliance, and understand product movement throughout the supply chain.

    Q3. What technologies are used for supply chain traceability?

    Common technologies include RFID, barcodes, QR codes, IoT sensors, GPS, cloud platforms, data analytics, and, in some use cases, blockchain.

    Q4. What is the difference between supply chain tracking and traceability?

    Tracking generally focuses on knowing where an item is or where it has moved. Traceability provides a broader record of an item’s history, including its origin, processing, movement, and associated supply chain information.

    Q5. How can businesses implement supply chain traceability?

    Businesses can start by identifying what needs to be tracked, selecting appropriate identification and monitoring technologies, integrating supply chain data, and continuously improving the system.

  • How Traceability Supports Faster Root Cause Analysis

    How Traceability Supports Faster Root Cause Analysis

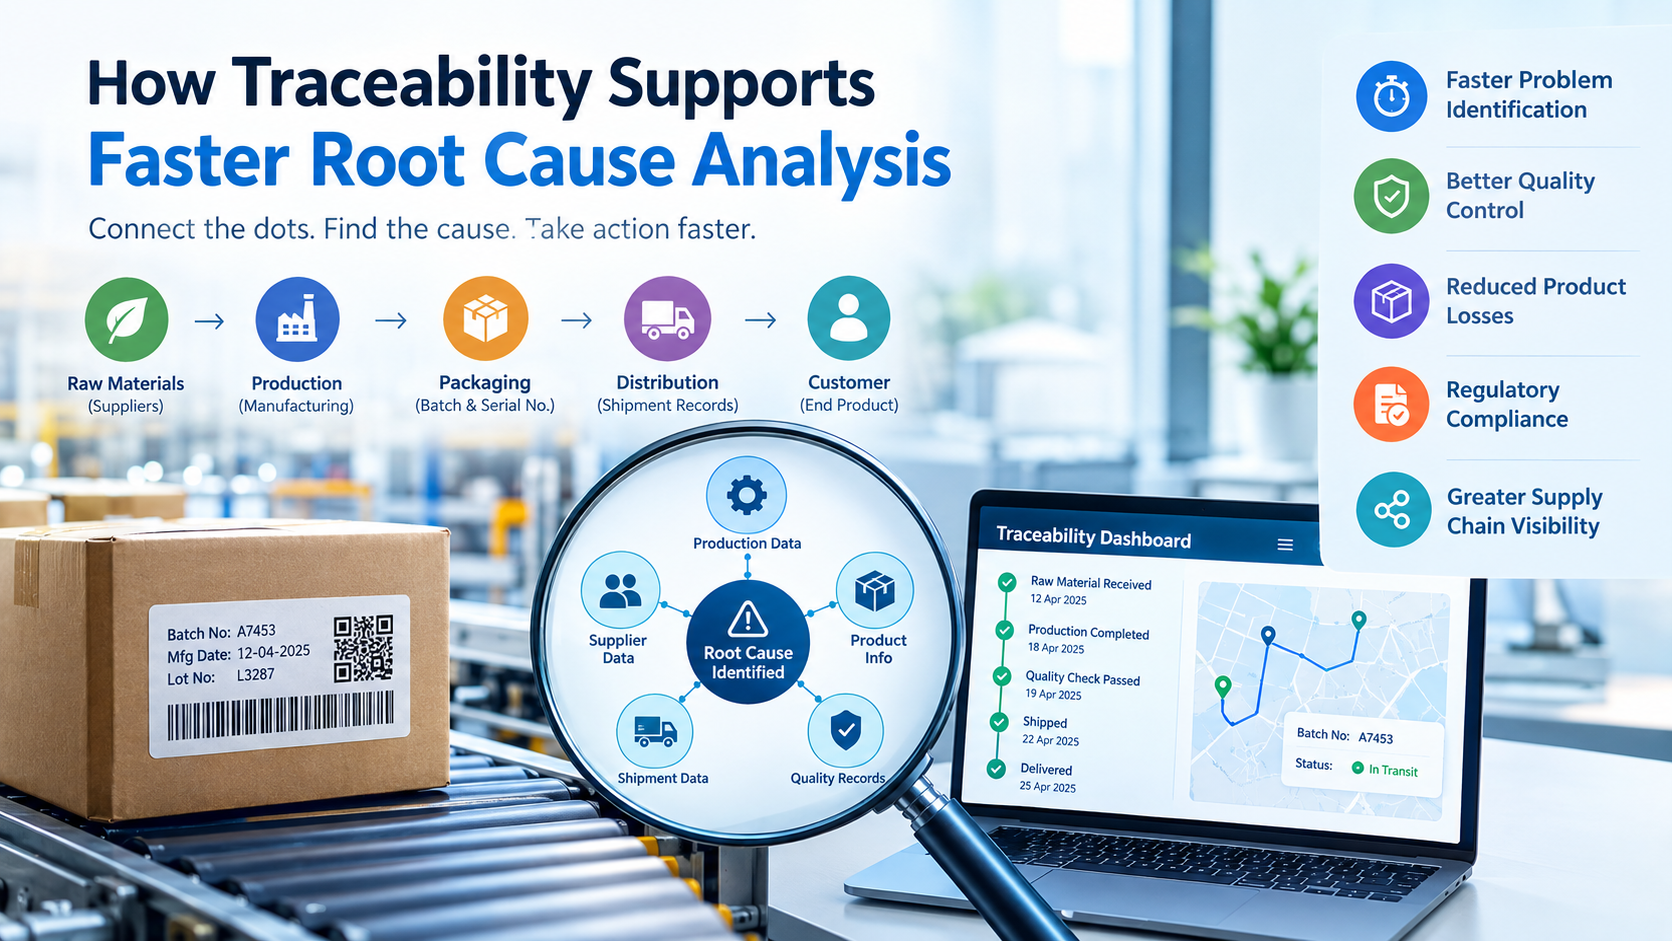
    When a product issue, quality failure, or supply chain problem occurs, businesses need to find the cause quickly. Delays in identifying the source of a problem can lead to product recalls, production downtime, customer complaints, and financial losses.

    This is where traceability for root cause analysis becomes important. A good traceability system allows businesses to follow products, materials, processes, and transactions throughout their journey. By connecting this information, companies can identify where a problem started and take corrective action faster.

    What Is Traceability in Root Cause Analysis?

    Understanding Traceability

    Traceability is the ability to track the history, location, movement, and status of a product, material, or process throughout the supply chain.

    For example, a manufacturer may need to know where a particular batch of raw materials came from, which production line processed it, when it was manufactured, and which customers received the finished products.

    A digital traceability system stores and connects this information, making it easier to access when an issue occurs.

    What Is Root Cause Analysis?

    Root cause analysis is a structured process used to identify the underlying reason behind a problem rather than only treating its visible symptoms.

    For example, if a batch of products fails a quality inspection, the business needs to determine whether the problem came from the raw material, production process, equipment, storage conditions, or another stage.

    How Traceability Connects the Two

    Traceability provides the historical data needed for root cause analysis. Instead of manually checking different records, teams can follow the product’s journey and identify where something went wrong.

    This can significantly reduce the time required to investigate a problem.

    Why Faster Root Cause Analysis Matters

    Reducing Product and Operational Risks

    A quality problem can affect multiple products or batches. Finding the source quickly helps businesses determine which products are actually affected and which are not.

    This allows companies to take targeted action instead of unnecessarily stopping an entire production process.

    Minimizing Downtime and Delays

    When the cause of a problem is unknown, production may need to be paused while teams investigate. Faster root cause analysis can help identify the affected process and reduce unnecessary downtime.

    Improving Quality and Compliance

    Many industries need detailed records about products, materials, and production processes. Traceability makes these records easier to access and supports quality management and regulatory requirements.

    How Traceability Supports Faster Root Cause Analysis

    Tracking Products Across the Supply Chain

    Traceability allows businesses to follow products from raw material sourcing through manufacturing, warehousing, distribution, and delivery.

    If a problem is detected, teams can trace the affected product backward to understand its history.

    Identifying the Source of a Problem

    A traceability system can connect products with important information such as batch numbers, suppliers, production lines, machines, operators, and processing dates.

    This helps teams narrow down the possible source of a problem much faster.

    Connecting Production and Quality Data

    Quality inspection results can be connected with production information. For example, if several defective products came from the same production line or batch, the data can help investigators identify a possible connection.

    Creating a Complete Audit Trail

    A complete audit trail provides a historical record of activities and events. It helps businesses understand what happened, when it happened, and where it happened.

    This information can make investigations more structured and evidence-based.

    Key Traceability Data Used for Root Cause Analysis

    Product and Batch Information

    Unique product IDs, batch numbers, serial numbers, and manufacturing dates can help identify specific products and groups that may be affected.

    Production and Manufacturing Records

    Production records can provide information about machines, production lines, processing times, temperatures, operators, and other relevant parameters.

    Supplier and Material Data

    Raw material information can help businesses trace a finished product back to its suppliers and original materials.

    If the same issue appears across products using materials from a particular source, this information can support further investigation.

    Distribution and Shipment Records

    Traceability also helps identify where affected products were shipped. Businesses can use this information to locate products in warehouses, distribution centers, or customer locations.

    How Digital Traceability Improves Root Cause Analysis

    Real-Time Data Collection

    Digital systems can collect information as products move through different stages. This provides businesses with more current information when investigating an issue.

    Automated Data Tracking

    Manual recordkeeping can be time-consuming and may introduce data-entry errors. Technologies such as RFID, barcodes, QR codes, and IoT devices can automate many tracking activities.

    Centralized Traceability Information

    A centralized system can bring product, production, quality, inventory, and shipment information together. Teams can then access relevant data without searching through multiple disconnected records.

    Faster Identification of Affected Products

    Once the source of a problem is identified, traceability data can help determine which products or batches may have been affected.

    This is particularly useful when businesses need to manage recalls or corrective actions.

    Traceability Technologies That Support Root Cause Analysis

    RFID Technology

    RFID uses radio-frequency identification to identify and track tagged products, assets, or materials. It can capture information without requiring direct line-of-sight scanning.

    This can improve visibility across warehouses, manufacturing facilities, and supply chains.

    Barcode and QR Code Tracking

    Barcodes and QR codes provide a simple way to identify products, batches, packages, and shipments. When connected to a digital system, scanning can create a record of product movement.

    IoT-Based Tracking

    IoT devices can collect information such as location, temperature, humidity, movement, and equipment conditions.

    This information can be particularly useful when environmental or operational conditions contribute to a product problem.

    Track and Trace Software

    Track and trace software connects identification, movement, production, inventory, and supply chain information in one system.

    It can provide businesses with a clearer view of product history and support faster investigations.

    Example of Traceability in Root Cause Analysis

    Identifying a Defective Product Batch

    Imagine a manufacturer discovers that a group of products has a quality problem.

    Without a digital traceability system, employees may need to manually check production records, supplier documents, inventory records, and shipment information.

    Tracing the Problem Back to Its Source

    With traceability, the business can use the product or batch ID to access its history.

    The system may show:

    • Raw material supplier
    • Material batch number
    • Production date
    • Production line
    • Machine information
    • Quality inspection results
    • Warehouse location
    • Shipment details

    By connecting this information, the investigation team can identify patterns and narrow down the possible source of the problem.

    Taking Corrective Action

    After identifying the likely source, the company can isolate affected products, investigate the underlying issue, correct the process, and monitor future production.

    The goal is not simply to find defective products but to understand why the problem occurred and prevent it from happening again.

    Benefits of Traceability for Root Cause Analysis

    Faster Problem Identification

    Connected traceability data can reduce the time required to locate the source of a problem.

    Better Quality Control

    Businesses can use historical and real-time information to identify quality issues and improve production processes.

    Reduced Product Losses

    Accurate traceability can help companies isolate affected products instead of treating an entire inventory as potentially defective.

    Improved Regulatory Compliance

    Detailed product and process records can support reporting, audits, recalls, and industry-specific compliance requirements.

    Better Supply Chain Visibility

    Traceability provides visibility across multiple stages of the supply chain, helping businesses understand how products and materials move from one point to another.

    Best Practices for Faster Root Cause Analysis

    Capture Data at Every Process Stage

    Businesses should collect relevant information from sourcing and manufacturing through warehousing, distribution, and delivery.

    Use Unique Product Identification

    Unique IDs, batch numbers, and serial numbers make it easier to connect products with their associated records.

    Automate Data Collection

    Using RFID, barcodes, QR codes, IoT sensors, and other technologies can reduce manual data entry and improve data availability.

    Maintain Accurate Records

    Traceability is only useful when the information is accurate and complete. Businesses should establish processes for maintaining reliable records.

    Monitor Traceability Data in Real Time

    Real-time visibility can help teams detect unusual events earlier and respond before a small issue becomes a larger problem.

    Conclusion

    Traceability for root cause analysis gives businesses the information they need to understand where problems begin and how they move through the supply chain.

    By connecting product, batch, production, quality, supplier, inventory, and shipment data, organizations can investigate problems more efficiently. Technologies such as RFID, barcodes, QR codes, IoT, and track and trace software can further improve data collection and visibility.

    A well-designed traceability system is therefore not only a way to track products. It can also become an important tool for quality improvement, risk management, corrective action, and continuous process improvement.

    Frequently Asked Questions

    Q1. How does traceability help with root cause analysis?

    Traceability provides historical information about products, materials, production processes, and shipments. This information helps teams identify where and when a problem may have started.

    Q2. What data is needed for root cause analysis?

    Useful data can include batch numbers, product IDs, supplier information, production records, machine information, quality results, inventory records, and shipment details.

    Q3. How does RFID improve traceability?

    RFID can automatically identify and track tagged products and assets, helping businesses collect movement and location data with less manual scanning.

    Q4. Can traceability reduce product recalls?

    Traceability can help businesses identify affected products and determine where they were distributed. This can support more targeted recall activities.

    Q5. What is the difference between tracking and traceability?

    Tracking generally focuses on knowing the current or historical location of an item. Traceability provides a broader history of a product, including its materials, processes, movements, and associated records.

  • The Business Value of End-to-End Product Visibility

    The Business Value of End-to-End Product Visibility

    In today’s competitive market, businesses need to know where their products are, what is happening to them, and when they will reach the customer. This is where end-to-end product visibility becomes important.

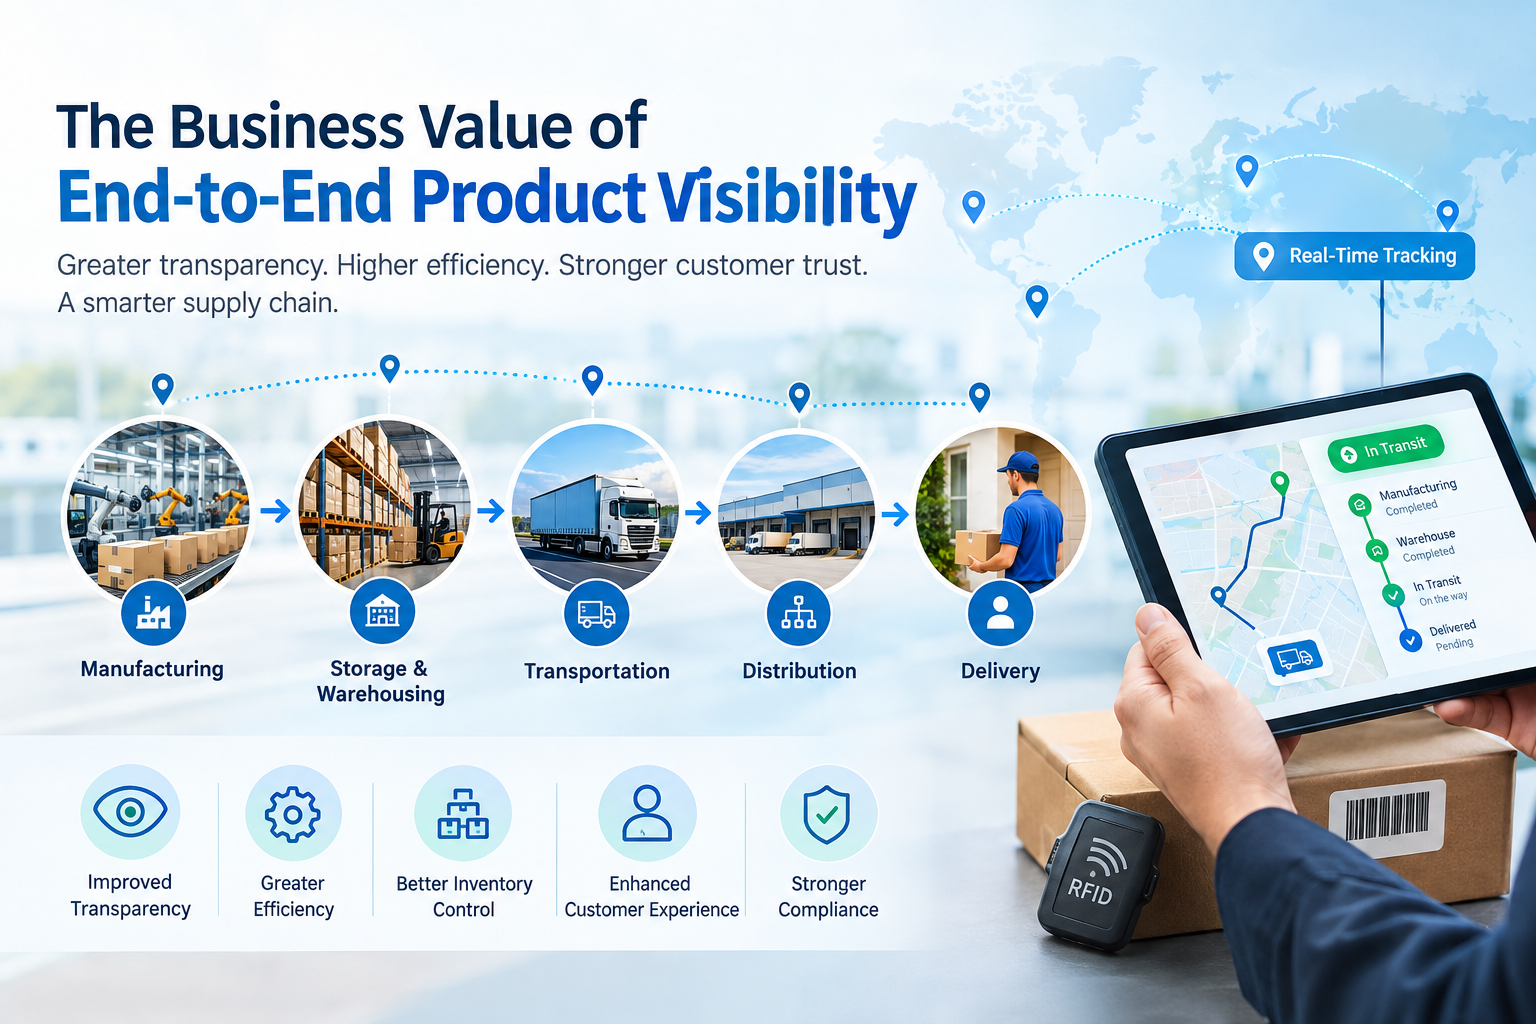
    End-to-end product visibility allows businesses to monitor products throughout their journey, from manufacturing and storage to transportation, distribution, and final delivery. With better visibility, companies can identify delays, manage inventory, improve customer service, and make faster business decisions.

    What Is End-to-End Product Visibility?

    End-to-end product visibility is the ability to track and monitor a product across its complete journey through the supply chain.

    Instead of relying on separate systems for manufacturing, warehousing, transportation, and delivery, businesses can connect information from different stages into a more complete view.

    For example, a manufacturer can monitor when a product is produced, stored in a warehouse, shipped to a distributor, and finally delivered to a customer.

    How End-to-End Product Visibility Works

    Product visibility combines tracking technologies, connected systems, and business data to provide information about products and their movement.

    A typical process can include:

    • Product identification
    • Production tracking
    • Warehouse monitoring
    • Shipment tracking
    • Distribution monitoring
    • Delivery confirmation
    • Data analysis and reporting

    When these stages are connected, businesses can gain a clearer understanding of their supply chain.

    Key Data Sources for Product Visibility

    Businesses can collect product and shipment information from several sources, including RFID tags, barcodes, IoT sensors, GPS devices, warehouse management systems, transportation management systems, and cloud platforms.

    Combining these sources helps businesses create a more connected view of product movement.

    Why End-to-End Product Visibility Matters for Businesses

    Limited visibility can make it difficult to understand where products are or why delays are occurring. Manual processes can also increase the possibility of errors.

    End-to-end product visibility helps businesses access relevant information across different supply chain stages.

    Improves Supply Chain Transparency

    Businesses can see product movements across manufacturing, warehousing, transportation, and delivery. This makes it easier to identify gaps and understand what is happening at different stages.

    Helps Reduce Delays and Operational Costs

    When businesses can identify delays early, they can take corrective action before problems become larger. Better visibility can also help reduce unnecessary handling, manual tracking, and inefficient processes.

    Supports Better Business Decisions

    Accurate and timely data allows managers to make informed decisions about inventory, transportation, production, and customer orders.

    Key Business Benefits of End-to-End Product Visibility

    Implementing product visibility can provide several operational and customer-facing benefits.

    Real-Time Product Tracking

    Businesses can monitor product locations and movement using technologies such as RFID, GPS, barcodes, and IoT devices.

    This can provide useful information about shipment status and help teams respond to unexpected events.

    Improved Inventory Management

    Better visibility helps businesses understand what inventory is available, where it is located, and how it is moving.

    This can support better stock management and reduce the risk of unnecessary inventory buildup or stock shortages.

    Faster Issue Detection and Resolution

    When a shipment is delayed or a product moves outside an expected process, visibility systems can help teams identify the issue more quickly.

    Early detection allows businesses to investigate and resolve problems before they significantly affect operations.

    Better Customer Experience

    Customers increasingly expect accurate information about their orders. Businesses with better product visibility can provide more reliable updates about order and delivery status.

    This improves communication and gives customers greater transparency.

    Improved Regulatory Compliance

    Some industries require detailed information about product movement, handling, and distribution.

    A connected visibility system can help businesses maintain records and provide traceability information when required.

    Technologies That Enable Product Visibility

    Modern product visibility depends on several technologies working together.

    RFID and Barcode Technology

    RFID and barcode systems provide businesses with ways to identify and track products.

    Barcodes are commonly scanned at different stages, while RFID can enable identification without requiring direct line-of-sight scanning in many use cases.

    IoT and Real-Time Tracking

    IoT devices can collect information about products, vehicles, equipment, and environmental conditions.

    For example, sensors can monitor location, temperature, humidity, or other conditions during transportation.

    Cloud-Based Data Platforms

    Cloud platforms can bring information from different systems together. This can make supply chain data easier to access, share, and analyze across business teams.

    AI and Data Analytics

    AI and analytics can help businesses identify patterns in supply chain data. Companies can use these insights to identify potential issues, analyze performance, and support more proactive decision-making.

    How End-to-End Product Visibility Improves Supply Chain Performance

    Visibility becomes particularly valuable when products move through multiple locations and business partners.

    From Manufacturing to Distribution

    During production, businesses can track products and associate them with relevant production information. Once products enter storage or distribution, tracking data can continue through the next stages.

    From Distribution to Delivery

    During transportation, businesses can monitor shipments and receive updates about their progress.

    This can help logistics teams identify delays and communicate more accurate information to customers and partners.

    Monitoring Products Across the Entire Journey

    The main value of end-to-end visibility comes from connecting different stages rather than monitoring each stage separately.

    A connected visibility approach can provide a more complete picture of the product journey.

    Challenges in Implementing End-to-End Product Visibility

    Although product visibility offers several benefits, implementation can involve challenges.

    Data Integration Challenges

    Businesses often use different software systems across departments and locations. Connecting these systems can require careful planning and integration.

    Implementation and Technology Costs

    Hardware, software, integration, training, and maintenance can create initial costs. Businesses need to select solutions that match their operational requirements.

    Data Security and Privacy

    Connected systems generate and share significant amounts of business data. Companies need appropriate security controls to protect sensitive information.

    Lack of Standardized Data

    Different suppliers, logistics providers, and internal departments may use different data formats and processes. Standardization can make information easier to combine and analyze.

    How Businesses Can Implement End-to-End Product Visibility

    Businesses can take a structured approach when developing a product visibility strategy.

    Identify Visibility Gaps

    Start by identifying where product information is currently unavailable, delayed, or difficult to access.

    Choose the Right Tracking Technologies

    Select technologies based on the products, environment, tracking requirements, and business objectives. Options may include RFID, barcodes, IoT sensors, GPS, or a combination of technologies.

    Integrate Data Across Business Systems

    Connect tracking data with relevant systems such as ERP, warehouse management, transportation management, and customer-facing platforms.

    Monitor and Optimize Performance

    After implementation, businesses should regularly review visibility data and identify opportunities to improve processes.

    Industries That Benefit From Product Visibility

    End-to-end product visibility can be useful across industries where products move through multiple supply chain stages.

    Manufacturing

    Manufacturers can track raw materials, work-in-progress items, finished products, and shipments.

    Healthcare and Pharmaceuticals

    Healthcare and pharmaceutical organizations can use traceability systems to monitor products and support controlled supply chains.

    Retail and E-Commerce

    Retailers can improve inventory visibility and provide customers with better order and delivery information.

    Logistics and Transportation

    Logistics companies can monitor shipments, vehicles, and delivery processes to improve operational visibility.

    Food and Agriculture

    Food and agriculture businesses can track products through production, storage, processing, distribution, and delivery.

    The Future of End-to-End Product Visibility

    Product visibility is moving toward more connected and automated supply chains.

    AI-Powered Supply Chain Visibility

    AI can analyze large volumes of supply chain data and help businesses identify patterns and potential operational issues.

    Predictive Analytics and Automation

    Predictive analytics can help companies understand possible future disruptions, while automation can reduce manual monitoring and repetitive tasks.

    Connected and Intelligent Supply Chains

    As RFID, IoT, cloud platforms, AI, and analytics continue to develop, businesses can build increasingly connected supply chains where product information is available across multiple stages.

    Conclusion

    End-to-end product visibility gives businesses a clearer view of how products move through the supply chain. From manufacturing and inventory to transportation and final delivery, connected visibility can help companies improve transparency, identify issues, manage inventory, and make better decisions.

    As supply chains become more complex, businesses can use technologies such as RFID, barcode systems, IoT, cloud platforms, and AI to build more connected and traceable operations.

    For companies looking to improve supply chain performance, product visibility is becoming an important part of creating efficient, responsive, and data-driven operations.

    Frequently Asked Questions

    Q1. What is end-to-end product visibility?

    End-to-end product visibility is the ability to monitor a product throughout its complete journey, from production and storage to transportation, distribution, and final delivery.

    Q2. Why is product visibility important for businesses?

    Product visibility helps businesses understand where products are, identify delays, manage inventory, improve supply chain transparency, and provide better information to customers.

    Q3. How does RFID improve product visibility?

    RFID can help businesses identify and track products using radio-frequency technology. It can support faster data collection and product monitoring across different operational stages.

    Q4. What technologies are used for product visibility?

    Common technologies include RFID, barcodes, IoT sensors, GPS tracking, cloud platforms, AI, analytics, ERP systems, warehouse management systems, and transportation management systems.

    Q5. How can businesses implement end-to-end product visibility?

    Businesses can begin by identifying visibility gaps, selecting suitable tracking technologies, integrating data across relevant systems, and continuously monitoring and improving their processes.

  • How Digital Records Improve Product History Management

    How Digital Records Improve Product History Management

    In today’s fast-moving business environment, knowing a product’s complete history is important for quality, compliance, and customer trust. Businesses need to know where a product was manufactured, how it moved through the supply chain, and whether it met required quality standards.

    Traditional paper-based records can make this information difficult to store, update, and retrieve. Digital Product History Management provides a better approach by storing product information electronically and making it easier to access, track, and manage.

    From manufacturing and healthcare to retail, logistics, and food production, digital records can improve product traceability and provide businesses with better control over their operations.

    What Is Product History Management?

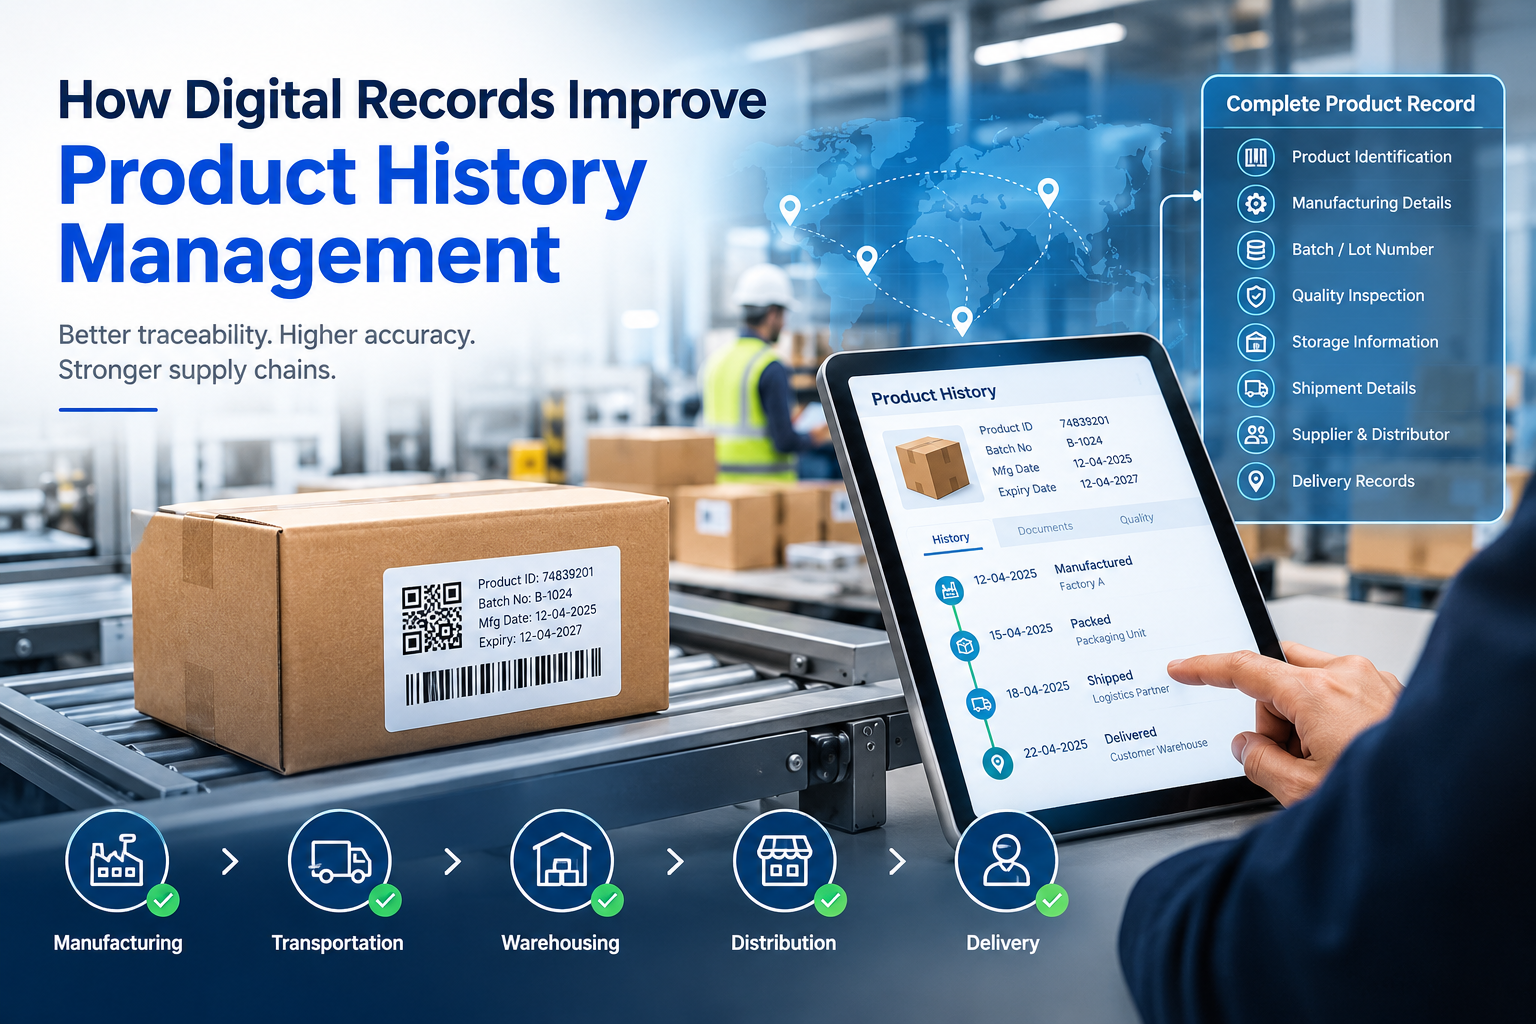
    Product history management is the process of recording and managing information about a product throughout its lifecycle. This may include manufacturing details, batch numbers, inspection records, transportation information, storage conditions, and delivery data.

    A complete product history helps businesses understand what happened to a product at every important stage.

    What Information Does a Product History Record Include?

    A product history record may contain:

    • Product identification number
    • Manufacturing date
    • Batch or lot number
    • Raw material information
    • Quality inspection results
    • Production records
    • Storage information
    • Shipment details
    • Supplier and distributor information
    • Delivery records

    Keeping this information organized allows businesses to quickly identify problems and understand the complete journey of a product.

    Why Accurate Product History Matters

    Accurate product history helps businesses maintain product quality and meet regulatory requirements. It also makes it easier to investigate product defects, manage recalls, and answer customer questions.

    Without reliable records, finding the source of a problem can take considerable time and may lead to inaccurate decisions.

    What Are Digital Records?

    Digital records are electronic versions of business and product information stored in databases, cloud platforms, enterprise software, or other digital systems.

    Instead of maintaining physical documents, businesses can record and update product information digitally.

    How Digital Product Records Work

    Digital records can collect information from different stages of the product lifecycle. Data can be entered manually or captured automatically using technologies such as barcodes, RFID, IoT devices, and automated software systems.

    The information can then be stored in a centralized system where authorized employees can access it when required.

    Digital Records vs. Paper-Based Records

    Paper records can be difficult to organize, search, update, and share. They can also be damaged or misplaced.

    Digital records provide faster access to information and make it easier to search, update, analyze, and share product data. Businesses can also create backups and apply access controls to protect important information.

    How Digital Records Improve Product History Management

    Digital records can transform the way businesses manage product information by improving visibility, accuracy, and accessibility.

    Improve Product Traceability

    Digital records make it easier to follow a product from manufacturing to distribution and delivery.

    Businesses can connect information from different stages and create a complete product history. This makes it easier to identify where a product came from and where it was delivered.

    Provide Real-Time Access to Product Information

    Authorized employees can access digital product information whenever they need it.

    For example, a warehouse employee can quickly check a product’s batch number, location, or shipment status without searching through physical files.

    Reduce Manual Errors

    Manual data entry and paper documentation can result in errors such as incorrect product numbers, missing information, or duplicate records.

    Automated data collection can reduce these errors and improve the reliability of product information.

    Improve Data Accuracy and Consistency

    Digital systems can standardize how product information is collected and stored.

    This helps businesses maintain consistent records across manufacturing facilities, warehouses, suppliers, distributors, and other locations.

    Support Regulatory Compliance

    Many industries need to maintain accurate records for compliance and auditing.

    Digital records can provide a clear history of product-related activities and make it easier to produce documentation when required.

    Make Audits Easier

    Searching through paper documents during an audit can be time-consuming.

    With digital records, businesses can quickly search for specific products, batches, transactions, or quality records. This can make the audit process more organized and efficient.

    Improve Supply Chain Visibility

    Digital product records connect information from different parts of the supply chain.

    Businesses can gain better visibility into production, inventory, transportation, and delivery activities, helping them identify delays and operational problems more quickly.

    Key Benefits of Digital Product History Management

    Implementing Digital Product History Management can provide several operational and business benefits.

    Faster Information Retrieval

    Employees can search digital databases and find product information much faster than searching through physical files.

    Better Inventory and Production Tracking

    Digital records can help businesses monitor products, batches, and inventory as they move through production and storage.

    Improved Quality Control

    Historical product information can help quality teams identify recurring problems and investigate defects more efficiently.

    Better Decision-Making

    Accurate historical data gives managers useful information for analyzing operations and making informed decisions.

    Increased Customer Trust

    Customers want businesses to provide safe, reliable, and traceable products. Maintaining accurate digital records can help companies provide greater transparency about product origins and handling.

    How Digital Records Support End-to-End Product Traceability

    Product traceability requires businesses to maintain information about a product throughout its journey.

    Digital records can connect this information and create a centralized product history.

    Tracking Products From Production to Delivery

    A product can be tracked through manufacturing, packaging, warehousing, transportation, and final delivery.

    Technologies such as RFID and barcode systems can automatically capture product movements and update digital records.

    Maintaining a Complete Product History

    Each important event can be added to the product record. This creates a timeline showing what happened to the product at different stages.

    A complete history can be particularly useful when investigating quality issues or product recalls.

    Connecting Product Data Across the Supply Chain

    Suppliers, manufacturers, logistics providers, warehouses, and distributors may all handle the same product.

    Digital systems can connect information from these different stages, providing better end-to-end visibility.

    Technologies Used for Digital Product Records

    Several technologies can support digital product history management.

    RFID and Barcode Technology

    RFID tags and barcodes provide unique identification for products, packages, assets, or shipments.

    Businesses can scan these identifiers to capture product information and update digital records.

    IoT and Real-Time Tracking

    IoT devices can collect information about product location, temperature, humidity, movement, and other conditions.

    This is particularly useful for products that require controlled storage or transportation.

    Cloud-Based Data Management

    Cloud platforms allow product information to be stored centrally and accessed by authorized users from different locations.

    This can help organizations manage product information across multiple facilities and supply chain partners.

    AI and Data Analytics

    AI and analytics can help businesses analyze historical product data and identify patterns.

    For example, companies may use data analysis to identify recurring quality problems, predict operational issues, or improve supply chain performance.

    Challenges of Implementing Digital Records

    Although digital records provide many benefits, businesses may face challenges during implementation.

    Data Security and Privacy

    Product information must be protected against unauthorized access, data loss, and cyber threats.

    Businesses should use appropriate security controls, authentication, backups, and access permissions.

    Integration With Existing Systems

    A company may already use ERP, warehouse management, manufacturing, or supply chain systems.

    The new digital record system should integrate with existing technology to avoid creating isolated data.

    Employee Training and Adoption

    Employees need to understand how to use new digital tools correctly.

    Proper training can help reduce mistakes and improve adoption across the organization.

    Initial Implementation Costs

    Moving from paper records to digital systems may require investment in software, hardware, employee training, and system integration.

    However, the long-term benefits can make digital transformation valuable for organizations that need better traceability and product visibility.

    Best Practices for Digital Product History Management

    Businesses can follow several practices to build an effective digital product history system.

    Standardize Product Data

    Create consistent formats for product IDs, batch numbers, dates, locations, and other important information.

    Use Unique Product Identification

    Use barcodes, RFID tags, serial numbers, or other identifiers to distinguish products and batches accurately.

    Keep Records Updated

    Product records should be updated whenever an important event occurs, such as production, inspection, shipment, receipt, or delivery.

    Secure and Back Up Product Data

    Use appropriate access controls and regular backups to protect important product information from unauthorized access or accidental loss.

    Future of Digital Product History Management

    The future of product history management will become increasingly connected and automated.

    Businesses are expected to use technologies such as AI, IoT, cloud computing, RFID, and advanced analytics to create more intelligent traceability systems.

    AI-Powered Traceability

    AI can analyze large volumes of product and supply chain data to identify unusual patterns and potential problems.

    IoT-Based Product Monitoring

    IoT sensors can provide real-time information about product location and environmental conditions, helping businesses monitor products throughout transportation and storage.

    Automated Compliance and Reporting

    Digital systems can automatically collect and organize records, making compliance reporting and audits more efficient.

    Conclusion

    Digital records are changing how businesses manage product information. By replacing disconnected paper documents with centralized digital systems, organizations can improve Digital Product History Management, product traceability, data accuracy, and supply chain visibility.

    Technologies such as RFID, barcodes, IoT, cloud platforms, and AI can further improve the way product information is captured and analyzed.

    For businesses that need reliable product traceability and better control over their supply chain, moving toward digital product records can be an important step toward more efficient and transparent operations.

    Frequently Asked Questions

    Q1. What is digital product history management?

    Digital product history management is the process of electronically recording, storing, and managing information about a product throughout its lifecycle.

    Q2. How do digital records improve product traceability?

    Digital records connect information from manufacturing, storage, transportation, and delivery, making it easier to track a product’s journey.

    Q3. What technologies are used to maintain digital product records?

    Common technologies include RFID, barcodes, IoT devices, cloud platforms, databases, and AI-powered analytics.

    Q4. Are digital product records better than paper records?

    Digital records are generally easier to search, update, share, analyze, and back up than paper records.

    Q5. How do digital records help businesses with compliance?

    Digital records provide organized and accessible documentation that can help businesses demonstrate product history, quality checks, and other required information during audits or compliance processes.

  • Centralized vs Distributed Traceability Systems

    Centralized vs Distributed Traceability Systems

    Centralized vs Distributed Traceability Systems: Which Is Better?

    Modern supply chains involve manufacturers, suppliers, distributors, warehouses, retailers, and customers. With so many participants involved, businesses need accurate and reliable ways to track products, materials, and information throughout the supply chain.

    This is where traceability systems become important. They help businesses record where products come from, where they are currently located, and what happens to them at different stages.

    Two common approaches are centralized and distributed traceability systems. While both are designed to improve visibility and data management, they work differently.

    In this article, we will explain the difference between centralized and distributed traceability systems, their advantages and limitations, use cases, and how businesses can choose the right approach.

    What Is a Traceability System?

    A traceability system is a technology-based solution that helps organizations track products, materials, assets, and related information throughout their lifecycle.

    It can collect information at different stages, including manufacturing, packaging, transportation, warehousing, distribution, and delivery.

    Businesses can use technologies such as RFID, barcodes, QR codes, IoT sensors, cloud platforms, and databases to collect and manage traceability data.

    How Traceability Systems Work

    A typical traceability system collects data whenever a product or asset moves through a supply chain.

    For example, a product may be:

    1. Manufactured at a production facility.
    2. Assigned a unique identification number.
    3. Stored in a warehouse.
    4. Transported to a distributor.
    5. Delivered to a retailer.
    6. Purchased by a customer.

    The system records important information at each stage, creating a traceable history of the product.

    Why Traceability Matters

    Effective traceability can help businesses improve:

    • Supply chain visibility
    • Product quality
    • Inventory management
    • Regulatory compliance
    • Product recalls
    • Operational efficiency
    • Customer confidence
    • Data-driven decision-making

    What Is a Centralized Traceability System?

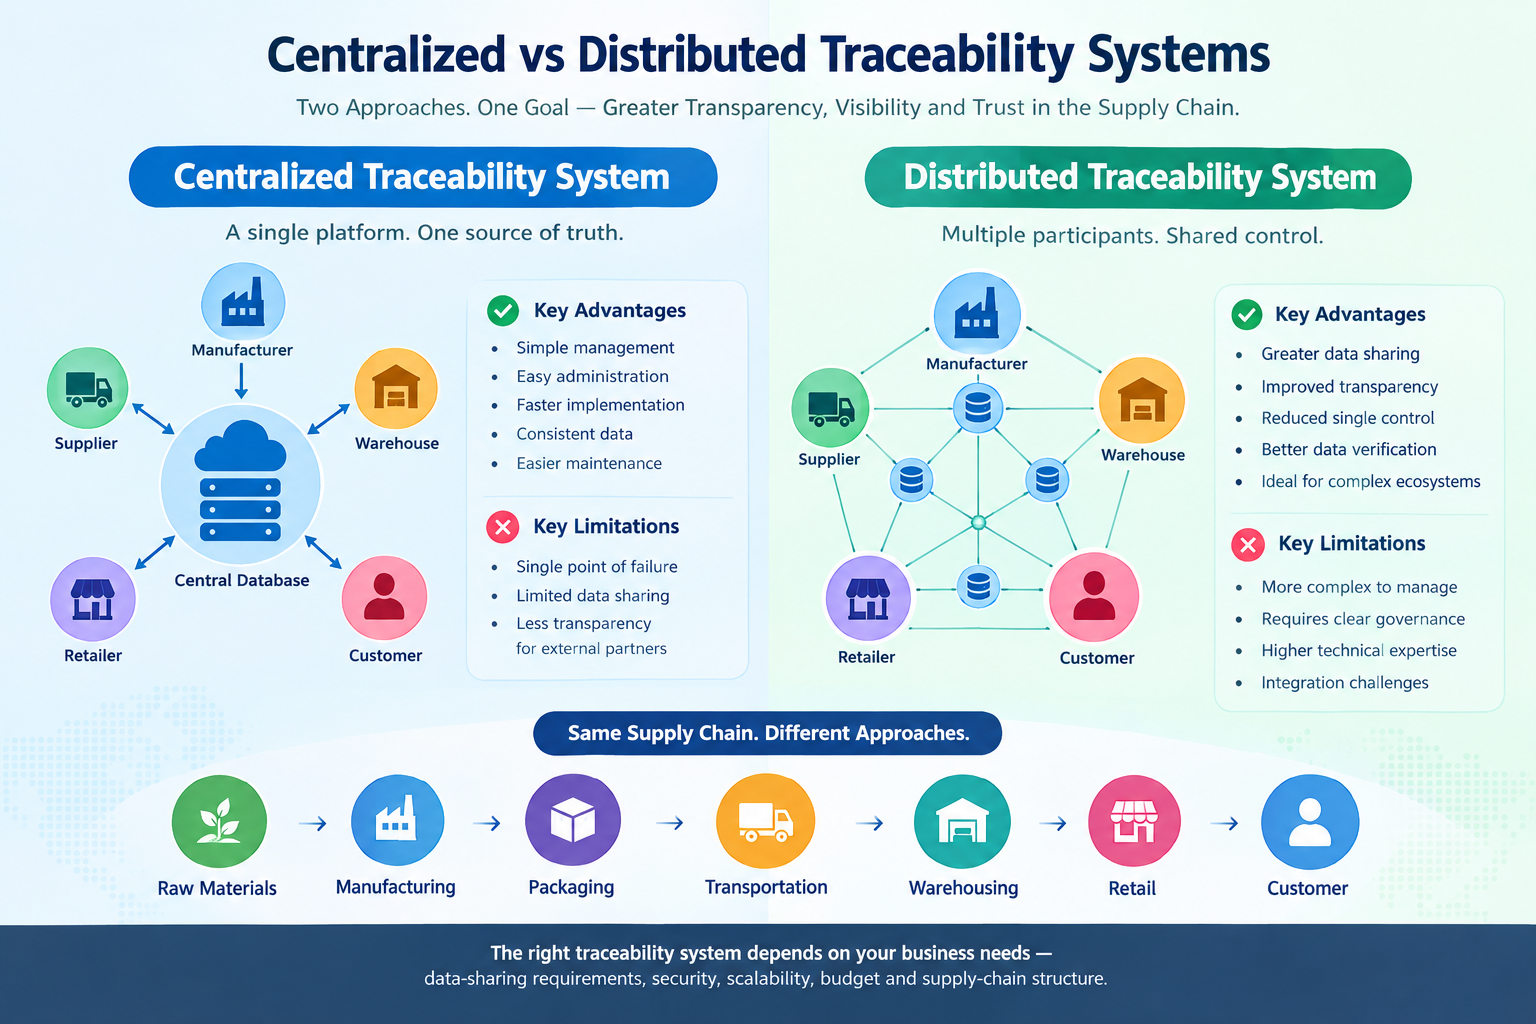
    A centralized traceability system stores and manages data through a central database or platform. A central organization or system administrator generally controls access, data management, and system operations.

    For example, a manufacturer may use one central cloud-based platform to collect information from its suppliers, warehouses, production facilities, and distribution partners.

    How Centralized Traceability Works

    In a centralized model, different users and devices send information to a central system.

    The central platform processes and stores the data. Authorized users can then access the information based on their permissions.

    This approach provides businesses with a single source of information for managing traceability data.

    Advantages of Centralized Traceability

    A centralized system can provide several benefits:

    • Simpler management: Data is managed from one central platform.
    • Easy administration: Organizations can control user access and permissions.
    • Faster implementation: Centralized systems can be easier to deploy within a single organization.
    • Consistent data management: Information follows centralized rules and processes.
    • Easier maintenance: Updates and system changes can be managed centrally.

    Limitations of Centralized Traceability

    Despite these advantages, centralized systems also have some limitations.

    A central database can become a critical point of failure. If the central platform experiences downtime, users may have difficulty accessing traceability information.

    There can also be challenges when multiple independent organizations need to share and verify data because control remains with the central authority.

    What Is a Distributed Traceability System?

    A distributed traceability system stores or manages information across multiple connected participants or nodes rather than depending entirely on one central authority.

    The goal is to allow different parties in a supply chain to participate in data sharing while maintaining greater distribution of control.

    Distributed approaches can use technologies such as distributed databases, blockchain, and other decentralized architectures.

    How Distributed Traceability Works

    In a distributed model, different participants can contribute or access relevant information according to predefined rules.

    For example, a manufacturer can record production information, a logistics company can record transportation data, and a retailer can record receiving information.

    Depending on the technology used, participants may be able to verify information without depending entirely on a single organization to maintain the complete record.

    Advantages of Distributed Traceability

    Distributed traceability can offer several benefits:

    • Greater data sharing: Multiple participants can contribute information.
    • Improved transparency: Authorized participants can have better visibility into shared records.
    • Reduced dependence on one central authority: Data management can be distributed across participants.
    • Better data verification: Some distributed architectures can help participants verify records.
    • Useful for complex ecosystems: It can be suitable when many independent organizations need to collaborate.

    Limitations of Distributed Traceability

    Distributed systems can also be more complex to design and manage.

    Organizations may need to establish clear rules about data ownership, access, governance, and interoperability.

    Implementation can also require more technical expertise, especially when blockchain or other advanced distributed technologies are involved.

    Centralized vs Distributed Traceability Systems: Key Differences

    Although both approaches support traceability, they differ in how information is stored, controlled, shared, and managed.

    Data Management

    A centralized system generally stores information in a central database.

    A distributed system spreads data management across multiple connected participants or nodes.

    Control

    Centralized systems normally have a central organization or administrator responsible for managing the platform.

    Distributed systems can distribute control among multiple participants depending on the architecture.

    Data Sharing

    Centralized systems can make internal data sharing straightforward because information is managed through one platform.

    Distributed systems can be useful when multiple independent organizations need to exchange and verify information.

    Security

    Centralized systems can use strong access controls, authentication, encryption, and monitoring. However, the central infrastructure becomes an important security target.

    Distributed systems can reduce reliance on one central point, but security still depends heavily on the technology, governance, permissions, and implementation.

    Scalability

    Centralized platforms can scale effectively when designed with modern cloud infrastructure.

    Distributed systems can also scale across participants, but adding more organizations can introduce additional governance and interoperability requirements.

    Cost and Maintenance

    Centralized solutions can be easier and less expensive to maintain when one organization controls the entire system.

    Distributed solutions may require additional infrastructure, integration, governance, and technical expertise.

    Centralized vs Distributed Traceability: Comparison Table

    Factor Centralized Traceability Distributed Traceability
    Data management Central database/platform Distributed across participants or nodes
    Control Central authority Shared or distributed
    Data sharing Usually controlled by central platform Designed for multi-party participation
    Implementation Generally simpler Can be more complex
    Maintenance Centrally managed Requires distributed governance
    Transparency Depends on access permissions Can provide shared visibility
    Security Centralized security controls Distributed security mechanisms
    Best suited for Organizations with centralized operations Complex multi-party ecosystems

    When Should You Choose a Centralized Traceability System?

    A centralized system can be a good choice when one organization needs strong control over its data and operations.

    Best Use Cases

    It may work well for:

    • Internal manufacturing operations
    • Warehouse management
    • Enterprise inventory tracking
    • Retail operations
    • Asset management
    • Organizations with centralized control

    For example, a manufacturer operating multiple warehouses may prefer a centralized platform that connects production, inventory, and distribution data in one place.

    Industries That Can Benefit

    Centralized traceability can be useful in industries such as:

    • Manufacturing
    • Retail
    • Healthcare
    • Logistics
    • Automotive
    • Food and beverage
    • Pharmaceuticals

    When Should You Choose a Distributed Traceability System?

    A distributed approach can be valuable when several independent organizations need to share information across a supply chain.

    Best Use Cases

    Distributed traceability can be considered for:

    • Global supply chains
    • Multi-party logistics networks
    • Product provenance
    • Cross-company traceability
    • Complex supplier networks
    • Industries requiring shared data verification

    For example, a food supply chain may involve farmers, processors, distributors, retailers, and regulators. A distributed approach can help different participants share relevant information across the product journey.

    Industries That Can Benefit

    Potential applications include:

    • Food and agriculture
    • Pharmaceuticals
    • Manufacturing
    • Logistics
    • Automotive
    • Consumer goods
    • Supply chain management

    Can Centralized and Distributed Systems Work Together?

    Yes. Businesses do not always have to choose between completely centralized or completely distributed architectures.

    A hybrid traceability system can combine centralized and distributed technologies.

    Hybrid Traceability Architecture

    For example, an organization can maintain its operational data in a centralized cloud platform while using a distributed technology layer to share selected information with external supply chain partners.

    This can provide centralized operational control while supporting broader data sharing.

    Benefits of a Hybrid Approach

    A hybrid model can help organizations achieve:

    • Centralized operational management
    • Controlled data sharing
    • Better interoperability
    • Improved supply chain visibility
    • Flexible system architecture
    • Support for different technology environments

    How to Choose the Right Traceability System

    The right approach depends on the organization’s business model, supply chain structure, technology requirements, and data-sharing needs.

    Consider Your Supply Chain Size

    A company with a relatively controlled supply chain may find a centralized system easier to manage.

    A large ecosystem involving many independent partners may require a more distributed approach.

    Evaluate Data Sharing Requirements

    Ask how many organizations need access to traceability information and how much data they need to share.

    If most information remains within one organization, centralized architecture may be sufficient.

    Consider Security and Compliance

    Businesses should evaluate data protection, access control, industry regulations, audit requirements, and data ownership before selecting an architecture.

    Evaluate Cost and Scalability

    Consider both initial implementation costs and long-term maintenance.

    The system should be able to grow as the organization adds products, locations, users, suppliers, and customers.

    Future of Traceability Systems

    Traceability is becoming increasingly connected with technologies such as IoT, artificial intelligence, cloud computing, RFID, and blockchain.

    IoT and Real-Time Tracking

    IoT sensors can collect information about location, temperature, humidity, movement, and other conditions.

    This can provide businesses with more real-time visibility into products and assets.

    AI-Powered Traceability

    Artificial intelligence can help analyze large volumes of traceability data and identify patterns, anomalies, delays, and potential risks.

    Blockchain and Distributed Data

    Blockchain can support certain distributed traceability applications by creating shared records that participants can verify according to the network’s rules.

    However, blockchain is not automatically the best solution for every traceability requirement.

    Cloud-Based Traceability

    Cloud platforms make it easier for businesses to connect locations, devices, applications, and supply chain partners through centralized infrastructure.


    Conclusion

    Both centralized and distributed traceability systems can help organizations improve supply chain visibility and product tracking. However, they address different business requirements.

    A centralized traceability system can be easier to manage and may be suitable for organizations that need centralized control. A distributed traceability system can be valuable for complex supply chains where multiple independent participants need to share information.

    Before choosing a solution, businesses should evaluate their supply chain structure, data-sharing requirements, security needs, scalability, budget, and compliance requirements.

    The best traceability architecture is not necessarily the most advanced one. It is the one that fits the organization’s actual operational and business needs.

    Frequently Asked Questions

    Q1. What is a centralized traceability system?

    A centralized traceability system manages traceability information through a central database or platform controlled by a central organization.

    Q2. What is a distributed traceability system?

    A distributed traceability system manages information across multiple connected participants or nodes, allowing data and control to be distributed depending on the architecture.

    Q3. What is the difference between centralized and distributed traceability?

    The main difference is how data and control are managed. Centralized systems depend primarily on a central platform, while distributed systems spread data management or control across multiple participants.

    Q4. Which traceability system is more secure?

    Neither architecture is automatically more secure. Security depends on system design, authentication, encryption, access controls, governance, monitoring, and implementation quality.

    Q5. Which traceability system is better for supply chains?

    There is no single answer. Centralized systems can be effective when one organization needs strong control, while distributed systems can be useful when multiple independent organizations need to share and verify information.

    Q6. Can a business use both centralized and distributed traceability?

    Yes. A hybrid architecture can combine centralized operational systems with distributed technologies for selected data-sharing or verification requirements.

  • What Makes a Track and Trace System Scalable?

    What Makes a Track and Trace System Scalable?

    As businesses grow, their supply chains become more complex. More products, suppliers, warehouses, shipments, and customers mean more data needs to be captured and managed. A basic tracking system may work for a small operation, but it can become difficult to manage as the business expands.

    This is where a scalable Track and Trace System becomes important. A scalable system can handle increasing data, users, locations, products, and transactions without affecting performance or visibility.

    But what exactly makes a Track and Trace System scalable? Let’s explore the key factors, technologies, benefits, and challenges involved.

    Why Scalability Matters in a Track and Trace System

    The Growing Need for Product Traceability

    Modern businesses need better visibility across the entire supply chain. They need to know where products are, where they came from, what processes they have passed through, and where they are going.

    As operations grow, manually managing this information becomes difficult. A scalable Track and Trace System helps businesses collect, organize, and access traceability data efficiently.

    What Does Scalability Mean in Traceability?

    Scalability means that a system can grow with the business.

    For example, a company may start by tracking a few thousand products from one warehouse. Later, it may need to track millions of products across multiple warehouses and countries.

    A scalable system should be able to support this growth without requiring a complete replacement of the technology.

    What Is a Scalable Track and Trace System?

    A Scalable Track and Trace System is a technology solution designed to track products, assets, shipments, and processes as business operations expand.

    It can support increasing numbers of products, users, locations, and data points while maintaining reliable performance.

    How a Track and Trace System Works

    A Track and Trace System generally collects information at different stages of the supply chain. Data can be captured using technologies such as barcodes, QR codes, RFID tags, IoT devices, and sensors.

    The collected information can then be stored and processed through software platforms, allowing businesses to monitor products and activities in real time.

    Key Features of a Scalable System

    A scalable system should provide:

    • Flexible architecture
    • Cloud-based infrastructure
    • Real-time data processing
    • Easy integration
    • Automated data collection
    • Strong security
    • Multi-location support
    • Reliable performance
    • Analytics and reporting

    These capabilities allow businesses to expand their tracking operations without creating unnecessary complexity.

    Key Factors That Make a Track and Trace System Scalable

    Flexible System Architecture

    A flexible architecture allows businesses to add new features, users, locations, and integrations as their requirements change.

    Instead of building a system that works only for today’s requirements, businesses should choose technology that can adapt to future needs.

    Cloud-Based Infrastructure

    Cloud technology can make scaling easier because businesses can increase computing and storage resources as their data requirements grow.

    Cloud-based Track and Trace Systems can also provide centralized access to information across different warehouses, offices, production facilities, and distribution centers.

    Real-Time Data Processing

    As the number of tracked products increases, the amount of data also grows.

    A scalable system should be capable of processing large amounts of information quickly. Real-time data processing helps businesses monitor inventory, shipments, production activities, and other supply chain operations.

    Easy Integration With Existing Systems

    Businesses rarely use only one software platform. They may already have ERP, WMS, CRM, inventory management, transportation management, or manufacturing systems.

    A scalable Track and Trace System should integrate with these platforms through APIs and other integration methods.

    This reduces data duplication and helps create a connected technology environment.

    Support for Increasing Data Volumes

    Every tracked product can generate multiple data points. When thousands or millions of products are involved, the volume of information can become significant.

    A scalable system needs suitable databases, data-processing capabilities, and storage infrastructure to manage this growth efficiently.

    Multi-Location and Global Scalability

    Growing businesses may operate across multiple warehouses, factories, stores, and distribution centers.

    A scalable system should allow organizations to manage traceability across multiple locations from a centralized platform while maintaining appropriate access controls.

    Automated Data Capture Technologies

    Manual data entry becomes increasingly difficult as operations grow.

    Technologies such as RFID, barcode scanning, QR codes, IoT sensors, and automated identification systems can capture information more efficiently and reduce manual errors.

    Technologies That Support Scalable Traceability

    RFID and Barcode Technology

    RFID and barcode technologies provide reliable ways to identify and track products and assets.

    Barcodes are commonly used for individual product identification, while RFID can enable automated identification without requiring direct line-of-sight scanning.

    IoT Sensors and Connected Devices

    IoT devices can collect real-time information about products, vehicles, equipment, and environmental conditions.

    For example, sensors can monitor location, temperature, humidity, or movement during transportation.

    Cloud Computing

    Cloud infrastructure provides flexible computing and storage resources. This makes it easier to support growing amounts of traceability data and increasing numbers of users.

    APIs and System Integration

    APIs allow different software applications to exchange information.

    For example, a Track and Trace System can exchange data with an ERP or warehouse management system, helping businesses maintain consistent information across platforms.

    AI and Data Analytics

    As traceability data increases, analytics can help businesses identify patterns, delays, anomalies, and operational problems.

    AI can also support predictive analysis and help organizations make faster, data-driven decisions.

    Challenges of Scaling a Track and Trace System

    Managing Large Volumes of Data

    More products and tracking events create more data. Without appropriate infrastructure, system performance can decline.

    Businesses should therefore plan their data storage and processing requirements before significant growth occurs.

    Integration With Legacy Systems

    Older business applications may not easily connect with modern Track and Trace platforms.

    Using APIs, middleware, or integration platforms can help overcome these challenges.

    Maintaining Data Accuracy

    Large-scale tracking is only useful when the underlying information is accurate.

    Automated data capture, validation processes, and regular system monitoring can help maintain data quality.

    Security and Compliance Requirements

    As more business and supply chain data is collected, security becomes increasingly important.

    Scalable systems should include appropriate authentication, authorization, encryption, monitoring, and data management practices.

    How Businesses Can Build a Scalable Track and Trace System

    Start With Clear Business Requirements

    Before implementing a system, businesses should identify what they need to track, where data will be collected, who will use it, and what information needs to be reported.

    Choose Flexible and Future-Ready Technology

    Businesses should select platforms that can support additional products, users, locations, devices, and integrations as operations expand.

    Plan for Business Growth

    Scalability should be considered from the beginning rather than after the system reaches its limits.

    Companies should estimate future data volumes, locations, transactions, and users when selecting their technology architecture.

    Focus on Integration and Interoperability

    A Track and Trace System should work with the existing technology ecosystem.

    Strong integration capabilities make it easier to connect different business systems and create a unified flow of information.

    Monitor and Optimize System Performance

    Regular performance monitoring helps identify bottlenecks before they become major problems.

    Businesses should review system speed, data processing, storage requirements, integrations, and user activity as operations grow.

    Benefits of a Scalable Track and Trace System

    Improved Supply Chain Visibility

    Businesses can gain better visibility into products, inventory, shipments, and processes across the supply chain.

    Better Operational Efficiency

    Automated tracking reduces manual work and can improve the efficiency of supply chain operations.

    Faster Decision-Making

    Real-time information allows teams to identify issues and respond faster.

    Reduced Errors and Product Losses

    Automated identification and tracking can reduce manual data-entry errors and improve product visibility.

    Support for Long-Term Business Growth

    The biggest advantage of scalability is flexibility. Businesses can expand their operations without having to replace their entire tracking infrastructure.

    Industries That Benefit From Scalable Traceability

    Manufacturing

    Manufacturers can track raw materials, work-in-progress products, finished goods, and production processes.

    Logistics and Transportation

    Logistics companies can monitor shipments, vehicles, packages, and delivery activities across multiple locations.

    Healthcare and Pharmaceuticals

    Healthcare and pharmaceutical organizations can use traceability to monitor products throughout the supply chain and support product identification and compliance requirements.

    Retail

    Retailers can track inventory movement from suppliers and warehouses to stores and customers.

    Food and Agriculture

    Food and agriculture businesses can improve visibility across production, processing, storage, and distribution.

    Conclusion

    A Scalable Track and Trace System is more than a tool for knowing where a product is. It is a technology foundation that helps businesses maintain visibility as their operations grow.

    Flexible architecture, cloud infrastructure, real-time processing, system integration, automated data capture, and strong security are some of the key elements that make a Track and Trace System scalable.

    By investing in scalable traceability technology, businesses can improve supply chain visibility, reduce manual processes, manage growing data volumes, and prepare their operations for future growth.

    Frequently Asked Questions

    Q1. What is a scalable Track and Trace System?

    A scalable Track and Trace System is a solution that can handle growing numbers of products, users, locations, and data without significantly affecting system performance.

    Q2. Why is scalability important in a Track and Trace System?

    Scalability allows businesses to expand their supply chain operations without replacing their tracking system. It helps manage increasing data volumes, products, warehouses, and users efficiently.

    Q3. What technologies make Track and Trace Systems scalable?

    Cloud computing, RFID, barcodes, QR codes, IoT sensors, APIs, automation, and data analytics can help make Track and Trace Systems more scalable and flexible.

    Q4. Can a Track and Trace System support multiple locations?

    Yes. A scalable Track and Trace System can support multiple warehouses, factories, stores, and distribution centers through a centralized platform.

    Q5. How does cloud technology improve Track and Trace scalability?

    Cloud technology provides flexible storage and computing resources that can be increased as business requirements grow. It also makes centralized access to traceability data easier.

    Q6. Can RFID and IoT be integrated with a Track and Trace System?

    Yes. RFID and IoT devices can automatically collect tracking information and send data to the Track and Trace platform, improving visibility and reducing manual data entry.

    Q7. What are the benefits of a scalable Track and Trace System?

    Key benefits include improved supply chain visibility, better operational efficiency, reduced manual errors, faster decision-making, easier integration, and support for long-term business growth.

    Q8. How can businesses choose a scalable Track and Trace System?

    Businesses should evaluate system architecture, integration capabilities, cloud support, data-processing capacity, security, automation features, and the ability to support future business growth.

  • How Traceability Data Moves Through the Supply Chain

    How Traceability Data Moves Through the Supply Chain

    A product does not simply move from a supplier to a customer. Before it reaches the customer’s hands, it may pass through manufacturers, warehouses, transportation providers, distributors, and retailers. At every stage, important information is created about the product and its movement.

    This is where supply chain traceability becomes important. Traceability allows businesses to understand where a product came from, what happened to it during production, where it has been stored, and how it reached its final destination.

    When this information is properly collected and connected, businesses can get better visibility into their supply chain, identify problems faster, improve product quality, and make more informed decisions.

    What Is Supply Chain Traceability?

    Supply chain traceability is the process of tracking a product, material, or component throughout its journey in the supply chain. It provides a record of important events, from the initial sourcing of raw materials to the delivery of the finished product.

    For example, a manufacturer may want to know where a particular batch of raw materials came from, when it entered production, which products were made from it, where those products were stored, and where they were eventually delivered.

    All of this information forms part of the product’s traceability record.

    What Is Traceability Data?

    Traceability data is the information collected as a product moves through different stages of the supply chain. It can include supplier details, product IDs, batch numbers, manufacturing dates, warehouse locations, shipment information, delivery records, and quality information.

    In some industries, businesses may also collect temperature, humidity, location, or other environmental data using sensors and IoT devices.

    The type of data collected depends on the product, industry, and requirements of the business.

    How Does Traceability Data Move Through the Supply Chain?

    Traceability data generally moves along with the physical movement of products.

    A simple supply chain can be represented as:

    Supplier → Manufacturer → Warehouse → Transportation → Distributor → Retailer → Customer

    At each stage, new information is created and added to the product’s digital record. When all these records are connected, businesses can follow the complete journey of a product.

    Data Begins With the Supplier

    The traceability journey usually starts with the supplier. When raw materials or components are purchased, the business can record information about their source.

    For example, a company may record the supplier’s name, material type, batch number, quantity, origin, and relevant certifications.

    This information becomes the starting point for tracking the material as it moves through the rest of the supply chain.

    Data Moves Into Manufacturing

    Once the raw materials arrive at a manufacturing facility, more information is added to the traceability record.

    The manufacturer can connect the raw-material batch with a particular production order or finished-product batch. Details such as production date, manufacturing process, quality inspection, and production location can also be recorded.

    This connection is especially useful when a company needs to find the source of a product problem. If a particular batch of finished products has a quality issue, the business can trace it back to the materials and production processes involved.

    Data Is Updated in the Warehouse

    After manufacturing, products are often moved to a warehouse or distribution center. The product’s location and movement can be recorded as it enters, moves through, and leaves the facility.

    For example, the system can record when a product was received, where it was stored, when it was picked for an order, and when it was dispatched.

    Technologies such as RFID, barcodes, QR codes, and warehouse management systems can make this process faster and reduce the need for manual data entry.

    Data Continues During Transportation

    The next stage is transportation. When products leave a warehouse, shipment information can be connected to their existing traceability records.

    Businesses can track information such as shipment numbers, vehicle details, departure times, destinations, delivery status, and transportation routes.

    For products that require controlled conditions, IoT sensors can provide additional information. For example, temperature-sensitive products may need to remain within a specific temperature range during transportation.

    This type of data can help businesses identify whether a product was exposed to unsuitable conditions during its journey.

    Data Reaches Distributors

    When products arrive at a distributor, the receiving information can be added to the traceability system.

    The distributor may record when the products were received, how many units arrived, where they were stored, and when they were sent to another location.

    This means the product’s history continues to grow as it moves between different supply-chain partners.

    Data Reaches Retailers

    Retailers are another important part of the traceability process. When products arrive at a store, warehouse, or fulfillment center, information about receiving and inventory can be recorded.

    Retailers can use this information to understand how much stock they have, where products are located, and when products were received or sold.

    For some products, retailers can also use QR codes to provide customers with additional information about the product.

    Data Reaches the Customer

    The final stage of the journey is the customer.

    Depending on the industry and the technology being used, customers may be able to access certain traceability information by scanning a QR code or using another digital method.

    They may be able to learn about the product’s origin, manufacturing details, certifications, authenticity, or other relevant information.

    This can increase transparency and help build trust between businesses and customers.

    Technologies That Help Move Traceability Data

    Modern supply chains use several technologies to collect and share traceability information. These technologies make it easier to connect physical products with digital records.

    RFID

    RFID, or Radio Frequency Identification, uses tags and readers to identify and track products and assets.

    It is particularly useful in warehouses and manufacturing environments because businesses can capture information about tagged items without manually scanning every individual product.

    Barcodes and QR Codes

    Barcodes are commonly used to identify products, packages, and shipments. When scanned, they can connect a physical item with information stored in a business system.

    QR codes work in a similar way but can also provide customers with access to additional digital information.

    IoT and Sensors

    IoT devices allow businesses to collect information from products, vehicles, equipment, and storage environments.

    For example, sensors can monitor temperature, humidity, location, movement, and other conditions. This is particularly useful for industries such as food, pharmaceuticals, healthcare, and cold-chain logistics.

    Cloud-Based Traceability Platforms

    Cloud-based platforms can bring information from different parts of the supply chain into a connected system.

    A business may have separate systems for manufacturing, inventory, warehousing, transportation, and sales. A traceability platform can help connect information from these systems and provide a broader view of the product journey.

    Blockchain

    Blockchain can be used to maintain a shared record of transactions and events between supply-chain participants.

    It can improve transparency and make historical records more difficult to change. However, blockchain is not necessary for every supply chain. Businesses should choose technologies based on their specific requirements.

    Why Is Supply Chain Traceability Important?

    The main value of traceability is visibility. Businesses can see what is happening to products and materials as they move through the supply chain.

    Faster Product Recalls

    Imagine a manufacturer discovers a problem with one particular batch of products. Without proper traceability, finding the affected products can take considerable time.

    With a good traceability system, the company can identify the relevant batch and determine where those products were shipped. This can make recalls faster and more targeted.

    Better Supply Chain Visibility

    Traceability gives businesses a clearer picture of product movement. Instead of relying on disconnected records, they can follow products across different stages of the supply chain.

    This can help identify delays, inventory problems, and other operational issues.

    Improved Quality Control

    When businesses can connect products with their suppliers, production processes, and batches, it becomes easier to investigate quality problems.

    Instead of looking at the entire supply chain, companies can focus on the specific stage or batch where an issue may have started.

    Better Regulatory Compliance

    Many industries have strict requirements for maintaining product and supply-chain records.

    A digital traceability system can make it easier to maintain, organize, and retrieve the information needed for compliance and audits.

    Reduced Counterfeiting

    Traceability can also support product authentication. By connecting products with unique identification numbers and digital records, businesses can make it more difficult for counterfeit products to enter legitimate supply chains.

    Challenges of Managing Traceability Data

    Although traceability provides many benefits, managing data across a complex supply chain can be challenging.

    Data Silos

    Different companies and departments may use different software systems. If these systems cannot communicate with each other, important information can remain isolated.

    This can create gaps in the product’s traceability record.

    Lack of Standardization

    Supply-chain partners may use different product codes, data formats, and identification methods.

    Without common standards, exchanging information between organizations can become difficult.

    Poor Data Quality

    Traceability is only useful when the data is accurate. Incorrect product numbers, missing information, duplicate records, or delayed updates can reduce the reliability of the system.

    Integration With Existing Systems

    Businesses often already have ERP, warehouse, manufacturing, and logistics systems in place.

    Connecting these systems to a modern traceability platform can require proper planning, integration, and technical expertise.

    Data Security

    Supply-chain information can contain sensitive business information. Companies therefore need appropriate security measures to control who can access and modify traceability data.

    How Businesses Can Improve Supply Chain Traceability

    Businesses do not necessarily need to completely replace their existing systems to improve traceability. They can start by identifying the most important products, processes, and data points that need to be tracked.

    Automate Data Collection

    Using RFID, barcode scanners, QR codes, and IoT devices can reduce manual data entry and improve the speed of data collection.

    Connect Different Systems

    Connecting manufacturing, inventory, warehouse, transportation, and traceability systems can help eliminate information gaps.

    Standardize Product Data

    Using consistent product IDs, batch numbers, shipment numbers, and data formats makes it easier for different systems and supply-chain partners to share information.

    Use Real-Time Monitoring

    Real-time monitoring can help businesses identify problems such as shipment delays, unexpected temperature changes, or inventory discrepancies before they become larger issues.

    Build End-to-End Visibility

    The ultimate goal of supply chain traceability should be to connect information from the original supplier all the way to the final customer.

    The more connected the data is, the easier it becomes for businesses to understand the complete product journey.

    The Future of Supply Chain Traceability

    Supply chain traceability is becoming more intelligent as businesses adopt technologies such as artificial intelligence, IoT, automation, and advanced analytics.

    AI can analyze large amounts of supply-chain data and help businesses identify unusual patterns, predict potential disruptions, and make better decisions.

    IoT devices can provide real-time information about products and shipments, while digital product passports can provide detailed information about products throughout their lifecycle.

    As businesses focus more on transparency, sustainability, compliance, and supply-chain resilience, the importance of connected traceability data will continue to grow.

    Conclusion

    Traceability data follows the journey of a product through the supply chain. It begins with information from suppliers, continues through manufacturing and warehousing, moves through transportation and distribution, and eventually reaches retailers and customers.

    When this information is collected accurately and connected across different stages, businesses gain better visibility into their operations.

    Technologies such as RFID, barcodes, QR codes, IoT sensors, cloud platforms, and data integration systems can make this process more efficient and reliable.

    Ultimately, supply chain traceability is not only about knowing where a product is. It is about understanding the complete journey of that product and having the right information available when businesses need it.

    Frequently Asked Questions

    Q1. What is supply chain traceability?

    Supply chain traceability is the ability to follow a product or material from its origin through manufacturing, storage, transportation, distribution, and delivery.

    Q2. How does traceability data move through the supply chain?

    Traceability data is collected whenever a product moves through a supply-chain stage. The information is then connected through digital systems to create a record of the product’s journey.

    Q3. What technologies are used for supply chain traceability?

    Common technologies include RFID, barcodes, QR codes, IoT sensors, cloud platforms, ERP systems, warehouse management systems, and blockchain.

    Q4. What is the difference between tracking and traceability?

    Tracking mainly focuses on the location and movement of an item, while traceability provides a broader view of the item’s history, including its origin, processing, movement, and related events.

    Q5. Why is supply chain traceability important?

    Supply chain traceability helps businesses improve visibility, quality control, inventory management, product recalls, compliance, and supply-chain risk management.

  • What Is a Track and Trace System and How Does It Work?

    What Is a Track and Trace System and How Does It Work?

    A Track and Trace System is a technology-based solution that helps businesses monitor the movement, location, and status of products, shipments, assets, and inventory throughout the supply chain. It provides businesses with better visibility into where an item is, where it has been, and where it is going.

    Modern track and trace solutions use technologies such as RFID, barcodes, QR codes, GPS, IoT sensors, cloud platforms, and analytics to collect and manage tracking information. These systems are widely used across manufacturing, logistics, healthcare, retail, pharmaceuticals, food, and other industries.

    What is a Track and Trace System?

    A Track and Trace System is a digital system designed to track the current location of an item and trace its movement throughout its lifecycle.

    Tracking focuses on determining the current location and status of a product, shipment, vehicle, or asset. Tracing focuses on understanding the item’s historical journey, including where it originated, which locations it passed through, and what processes it went through.

    For example, when a product moves from a manufacturer to a warehouse and then to a retailer, a track and trace system can record each stage. Businesses can use this information to monitor shipments, identify delays, manage inventory, and investigate problems.

    Definition of a Track and Trace System

    In simple terms, a track and trace system answers two important questions:

    • Where is the item now?
    • Where has the item been?

    The system collects information at different points in the supply chain and stores it in a centralized platform. Authorized users can then access this information to monitor operations and make better decisions.

    Why Is Track and Trace Important for Businesses?

    Supply chains can involve manufacturers, suppliers, warehouses, transporters, distributors, retailers, and customers. Without proper visibility, it can become difficult to identify where products are located or why shipments are delayed.

    A track and trace system provides greater visibility and helps businesses:

    • Monitor products and shipments in real time
    • Improve inventory accuracy
    • Reduce losses and misplaced items
    • Identify supply chain delays
    • Improve customer service
    • Support regulatory compliance
    • Maintain product history and traceability

    How Does a Track and Trace System Work?

    A Track and Trace System generally works by identifying an item, collecting data about it, transmitting that data to a centralized platform, and making the information available for monitoring and analysis.

    Step 1: Product Identification

    The first step is assigning a unique identification number or digital identity to a product, shipment, asset, or package.

    Businesses may use:

    • RFID tags
    • Barcodes
    • QR codes
    • Serial numbers
    • GPS devices
    • IoT-enabled sensors

    This unique identification allows the system to distinguish one item from another.

    Step 2: Data Capture

    Once the item is identified, tracking information is captured at different points in the supply chain.

    For example, an RFID reader can automatically detect a tagged product when it enters a warehouse. Similarly, employees can scan a barcode when a shipment is dispatched.

    The collected information may include:

    • Product ID
    • Location
    • Date and time
    • Shipment status
    • Quantity
    • Temperature or environmental conditions
    • Movement history

    Step 3: Data Transmission

    The captured data is transmitted to tracking software or a centralized database.

    Depending on the system, data can be transferred using technologies such as Wi-Fi, cellular networks, Bluetooth, GPS, or other IoT communication technologies.

    Step 4: Real-Time Tracking

    The tracking platform processes incoming data and provides visibility into the current status and location of items.

    For example, a logistics company can monitor whether a shipment is:

    • In transit
    • At a warehouse
    • Delayed
    • Delivered
    • Returned

    This information can be displayed through dashboards, mobile applications, or web-based platforms.

    Step 5: Data Monitoring and Reporting

    The final step involves analyzing collected information to identify trends, delays, exceptions, and operational issues.

    Businesses can generate reports and alerts to improve supply chain performance and take corrective action when necessary.

    Key Components of a Track and Trace System

    A modern track and trace solution usually combines multiple hardware and software technologies.

    RFID Technology

    Radio Frequency Identification (RFID) uses radio waves to identify and track tagged objects. RFID can help businesses automatically capture information without requiring direct line-of-sight scanning.

    It is commonly used for inventory management, asset tracking, warehouse operations, and supply chain visibility.

    Barcode and QR Code Technology

    Barcodes and QR codes are widely used because they are relatively simple and cost-effective.

    A barcode or QR code can contain information associated with a product or shipment. Scanning the code allows the system to retrieve relevant information and update its status.

    GPS Tracking

    GPS technology is particularly useful for monitoring vehicles and shipments during transportation.

    Businesses can use GPS tracking to monitor vehicle locations, delivery routes, estimated arrival times, and potential transportation delays.

    IoT Sensors

    IoT sensors can collect information beyond location. Depending on the application, sensors can monitor temperature, humidity, vibration, pressure, and other environmental conditions.

    This can be particularly useful for sensitive products such as pharmaceuticals, food, and certain industrial materials.

    Cloud-Based Tracking Software

    Cloud-based platforms provide a centralized environment where tracking data can be stored, processed, analyzed, and accessed by authorized users.

    Businesses can use dashboards to view supply chain activity and generate reports without relying on disconnected tracking systems.

    Benefits of a Track and Trace System

    Implementing a Track and Trace System can provide several operational and strategic benefits.

    Improved Supply Chain Visibility

    Businesses gain greater visibility into the movement of products and shipments. This makes it easier to identify delays, bottlenecks, and operational problems.

    Real-Time Product Tracking

    Real-time tracking allows businesses to monitor the status and location of products or shipments as they move through the supply chain.

    Reduced Product Loss and Theft

    Tracking systems create a digital record of product movements. This can help organizations identify missing inventory and investigate unauthorized movement.

    Better Inventory Management

    Accurate tracking information can help businesses understand inventory levels and locations, reducing the risk of overstocking, stockouts, and misplaced products.

    Improved Regulatory Compliance

    Some industries require detailed records of product movement and history. Track and trace systems can help businesses maintain accurate records and support compliance requirements.

    Increased Operational Efficiency

    Automating data collection and tracking processes can reduce manual work and improve the speed and accuracy of supply chain operations.

    Track and Trace System in Different Industries

    Track and Trace in Manufacturing

    Manufacturers can use track and trace systems to monitor raw materials, work-in-progress inventory, finished goods, and assets.

    The system can help organizations identify where materials are being used and trace products through different production stages.

    Track and Trace in Logistics and Transportation

    Logistics companies can track shipments, vehicles, containers, and delivery routes.

    Real-time visibility can help logistics providers identify delays and provide customers with more accurate shipment information.

    Track and Trace in Healthcare and Pharmaceuticals

    Healthcare and pharmaceutical organizations can use track and trace systems to monitor medicines, medical equipment, and other products.

    Tracking can help improve product visibility, support inventory management, and strengthen product traceability.

    Track and Trace in Retail

    Retail businesses can track products from distribution centers to stores and customers.

    This helps retailers improve inventory accuracy, manage replenishment, and monitor product movement across locations.

    Track and Trace in Food and Beverage

    Food businesses can use traceability systems to monitor products from suppliers through processing, distribution, and retail.

    This can make it easier to identify the source and distribution path of products when quality or safety issues occur.

    Track and Trace System vs. Traditional Tracking

    Traditional tracking methods often depend heavily on manual data entry, spreadsheets, paperwork, phone calls, or disconnected systems.

    Modern track and trace platforms can automate much of the data collection and provide centralized visibility.

    Traditional Tracking Methods

    Traditional methods may involve:

    • Manual record keeping
    • Paper-based documentation
    • Phone-based status updates
    • Spreadsheet tracking
    • Limited shipment visibility

    These methods can increase the risk of human errors and make real-time monitoring difficult.

    Modern Track and Trace Systems

    Modern systems combine identification technologies, connected devices, software platforms, and analytics to provide more automated visibility.

    Businesses can monitor product movement and access historical tracking information from a centralized platform.

    Why Businesses Are Moving to Digital Track and Trace

    Growing supply chain complexity has increased the need for accurate and timely information. Digital track and trace systems can help businesses replace fragmented processes with more connected and transparent operations.

    Challenges of Implementing a Track and Trace System

    Although track and trace technology offers many advantages, businesses may face challenges during implementation.

    Integration With Existing Systems

    A new tracking platform may need to integrate with ERP, warehouse management, transportation management, inventory, or other business systems.

    Data Security and Privacy

    Tracking systems can collect significant amounts of operational data. Businesses need appropriate security controls to protect sensitive information.

    Implementation Cost

    Hardware, software, integration, maintenance, and employee training can contribute to the overall implementation cost.

    Employee Training

    Employees may need training to operate scanners, RFID readers, mobile applications, dashboards, and other components of the system.

    Data Accuracy and Quality

    A track and trace system is only as effective as the data it receives. Incorrect product IDs, missing scans, damaged tags, or incomplete information can affect tracking accuracy.

    How to Choose the Right Track and Trace System

    Businesses should evaluate their operational requirements before selecting a tracking solution.

    Define Your Tracking Requirements

    Determine what needs to be tracked, such as products, inventory, vehicles, shipments, containers, or assets.

    Consider Scalability

    Choose a system that can support increasing product volumes, additional locations, users, and future business requirements.

    Check Technology Integration

    The solution should be capable of integrating with existing business applications and databases.

    Evaluate Real-Time Visibility

    If real-time monitoring is important, evaluate the system’s ability to provide timely location and status information.

    Consider Security and Compliance

    Businesses should evaluate authentication, access controls, data protection, reporting capabilities, and industry-specific compliance requirements.

    Future of Track and Trace Systems

    The future of Track and Trace Systems is closely connected with AI, IoT, automation, cloud computing, and advanced analytics.

    AI-Powered Tracking

    Artificial intelligence can analyze tracking data to identify patterns, predict potential delays, and support more informed supply chain decisions.

    IoT-Based Supply Chain Visibility

    Connected IoT devices can continuously collect information about products, vehicles, environmental conditions, and assets.

    Predictive Analytics

    Predictive analytics can help businesses identify potential supply chain disruptions before they significantly affect operations.

    Blockchain for Product Traceability

    Blockchain technology can provide a distributed record of transactions and product movements, potentially improving transparency and data integrity in suitable applications.

    Automated Tracking and Reporting

    Automation can reduce manual tracking activities and enable systems to generate alerts, reports, and updates based on predefined conditions.

    Conclusion

    A Track and Trace System provides businesses with greater visibility into the movement and history of products, shipments, assets, and inventory. By combining technologies such as RFID, barcodes, GPS, IoT sensors, cloud platforms, and analytics, businesses can improve tracking accuracy and supply chain visibility.

    As supply chains become increasingly digital and complex, track and trace technology will continue to play an important role in improving operational efficiency, inventory management, transparency, compliance, and customer service.

    Frequently Asked Questions About Track and Trace Systems

    Q1. What is a Track and Trace System?

    A Track and Trace System is a technology solution that helps businesses monitor the location, status, and movement history of products, shipments, assets, or inventory throughout their lifecycle.

    Q2. How does a Track and Trace System work?

    A Track and Trace System identifies an item, captures tracking data, transmits the information to a centralized platform, and provides users with current and historical visibility.

    Q3. What technologies are used in Track and Trace Systems?

    Common technologies include RFID, barcodes, QR codes, GPS, IoT sensors, cloud platforms, databases, mobile applications, and analytics.

    Q4. What are the benefits of a Track and Trace System?

    Major benefits include improved supply chain visibility, real-time tracking, better inventory management, reduced losses, improved operational efficiency, and stronger product traceability.

    Q5. Which industries use Track and Trace Systems?

    Manufacturing, logistics, transportation, healthcare, pharmaceuticals, retail, food and beverage, automotive, and other industries can use track and trace technology.

    Q6. What is the difference between tracking and tracing?

    Tracking generally focuses on the current location or status of an item, while tracing focuses on understanding its historical journey, origin, and movement through different stages.